



Injection Molding Mold Parts: Noyau, Cavité, Éjection, and Guide Parts
Injection molding mold parts include the core, cavity, Système d’éjection, Composants du guide, runners, gates, cooling channels, and venting features. These systems work together to shape plastic parts, maintain alignment, control resin flow, and release finished products safely. High-quality mold components improve dimensional accuracy, Réduction de l’usure, prevent defects like flashing or sticking, and help manufacturers maintain stable production across long production runs.
Injection molds work as complete systems, but every system depends on the quality of its individual parts. A worn guide bushing, poorly positioned ejector pin, or inefficient cooling channel can create defects even when the rest of the mold looks fine. Understanding how these components work together helps engineers, buyers, and production teams make better tooling decisions and avoid expensive downtime later.
What are the main parts of an injection molding mold?
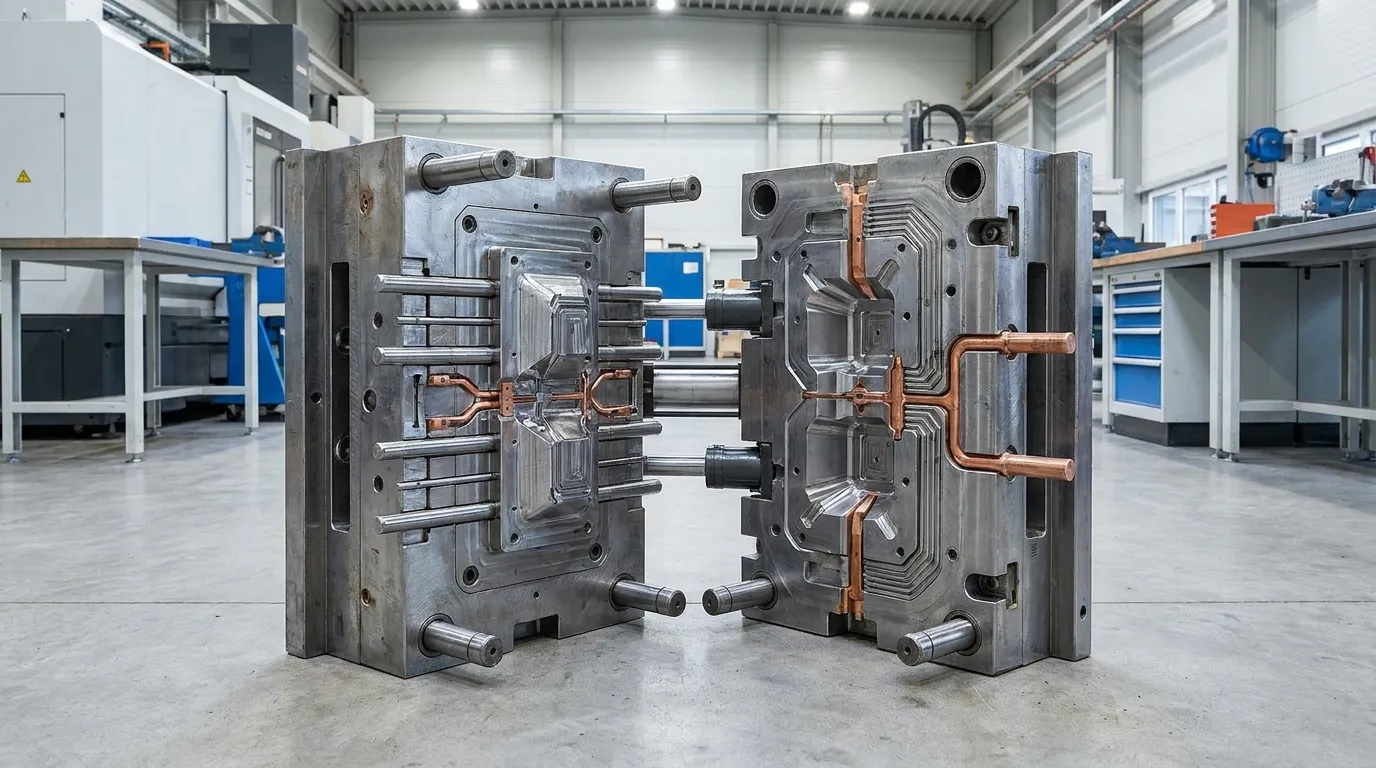
Injection molding mold parts are usually grouped into forming, Alignement, Éjection, Refroidissement, and flow-control systems. Each group affects part quality, mold life, and production consistency in different ways.
Most injection molds contain the same core component groups, even when part designs vary. The core and cavity create the molded shape, alignment parts keep mold halves positioned correctly, and ejection systems remove cooled parts after molding. Canaux de refroidissement, runners, and gates manage heat and resin flow throughout the cycle.
If you need a broader breakdown of complete mold architecture, Ceci Aperçu des composants du moule explains how these systems connect inside a full tooling setup.
Selon le Aperçu Wikipédia du moulage par injection, standard molds also include venting features, mold plates, and clamping systems that support pressure and alignment during production.
Table de fonction des composants du moule d’injection
| Groupe des composants | Fonction principale | Risque de défaillance courant | Production Impact |
|---|---|---|---|
| Noyau et cavité | Géométrie des pièces de forme | Usure et décalage | Flashing, dimensional errors |
| Système de guides | Maintenir l’alignement | Usure des bagues | Défauts de ligne de séparation |
| Système d’éjection | Retirer les pièces moulées | Dégâts de goupille | Scratches, Stuck |
| Système de glissières et de portails | Écoulement direct de résine | Usure de la porte | Plans courts, imbalance |
| Système de refroidissement | Contrôler la température du moule | Mauvais débit de refroidissement | Déformation, long cycle times |
| Système de ventilation | Libérez de l’air piégé | Bouches d’aération | Marques de brûlure, incomplete filling |
What is the difference between the core and cavity?
The cavity forms the external shape of the plastic part, while the core creates internal features and hollow sections. Both must stay precisely aligned to avoid flash, warping, or dimensional defects.
The cavity side usually creates the visible outside surface of the molded part. The core side forms internal details such as holes, Côtes, or mounting structures. During injection, molten resin fills the space between these two surfaces to create the finished component.
Un détail Bases du moule d’injection guide can help if you want to understand how the full molding cycle supports these forming surfaces.
| Caractéristiques | Noyau | Cavité |
|---|---|---|
| Rôle principal | Crée une géométrie interne | Crée une forme extérieure |
| Exposition | Haute pression et friction | Exigences élevées en finition de surface |
| Problème d’usure courant | Abrasion et collage | Rayures de surface |
| Impact sur la qualité | Dimensions internes | Apparence esthétique |
The core often experiences higher mechanical stress because parts shrink around it during cooling. This is why ejector placement matters so much. If the core surface grips the plastic too tightly, the ejection system can damage the finished part during release.
Par exemple, medical device housings often require highly polished cavity surfaces to maintain cosmetic quality. En même temps, the core may need hardened steel inserts to resist wear from repeated production cycles.
Which mold parts control alignment and precision?
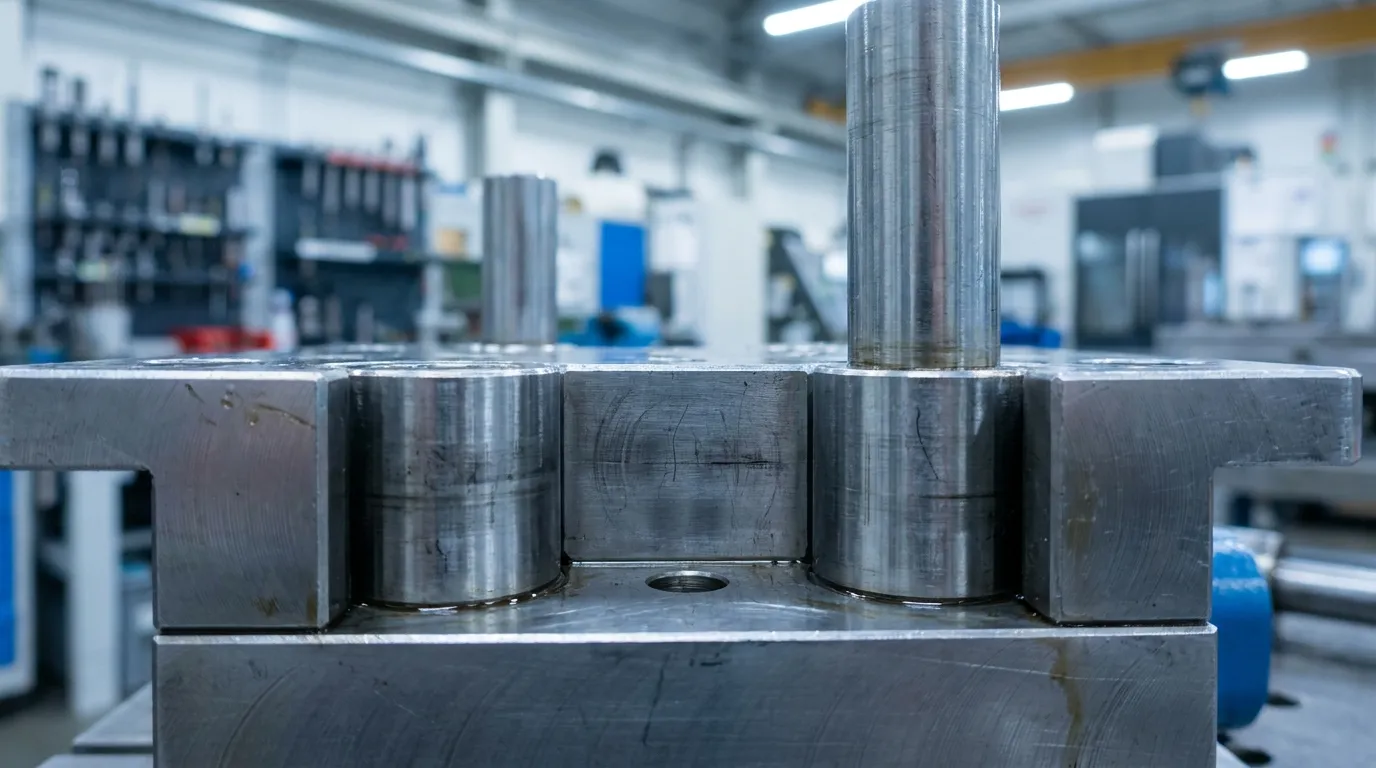
Guide posts and bushings keep mold halves aligned during every cycle. Poor alignment increases wear, flashing, part mismatch, and long-term tooling instability.
Alignment systems control how accurately the mold closes during production. Even slight misalignment can create flashing at the parting line or uneven pressure across the cavity surface. Over time, this accelerates mold wear and reduces dimensional consistency.
Le Composants du guide section explains how precision alignment parts support repeatable molding performance.
Selon le Guide des composants de moule Agilian, guide pins and bushings are among the most important wear surfaces inside production tooling.
Table d’échec d’alignement si et alors
| Si cela arrive | Cause probable | Résultat de la production |
|---|---|---|
| Flashing à la ligne de séparation | Silents guides usés | Fuite excessive de résine |
| Pression inégaire dans la cavité | Moitiés de moule désalignées | Distorsion des parties |
| Usure rapide des bords de cavité | Faible répétabilité de l’alignement | Durée de vie réduite du moule |
| Désaccord de surface | Poteaux guides endommagés | Défauts visibles des pièces |
Lower-cost guide systems are not always the best long-term option. They may work for short production runs, but high-cycle molds usually need hardened alignment components to maintain precision over time.
An automotive interior trim mold is a good example. After extended production cycles, worn guide bushings often create flashing along visible edges. Replacing only the cavity inserts rarely fixes the issue if alignment wear caused the original problem.
How does the ejection system remove molded parts?
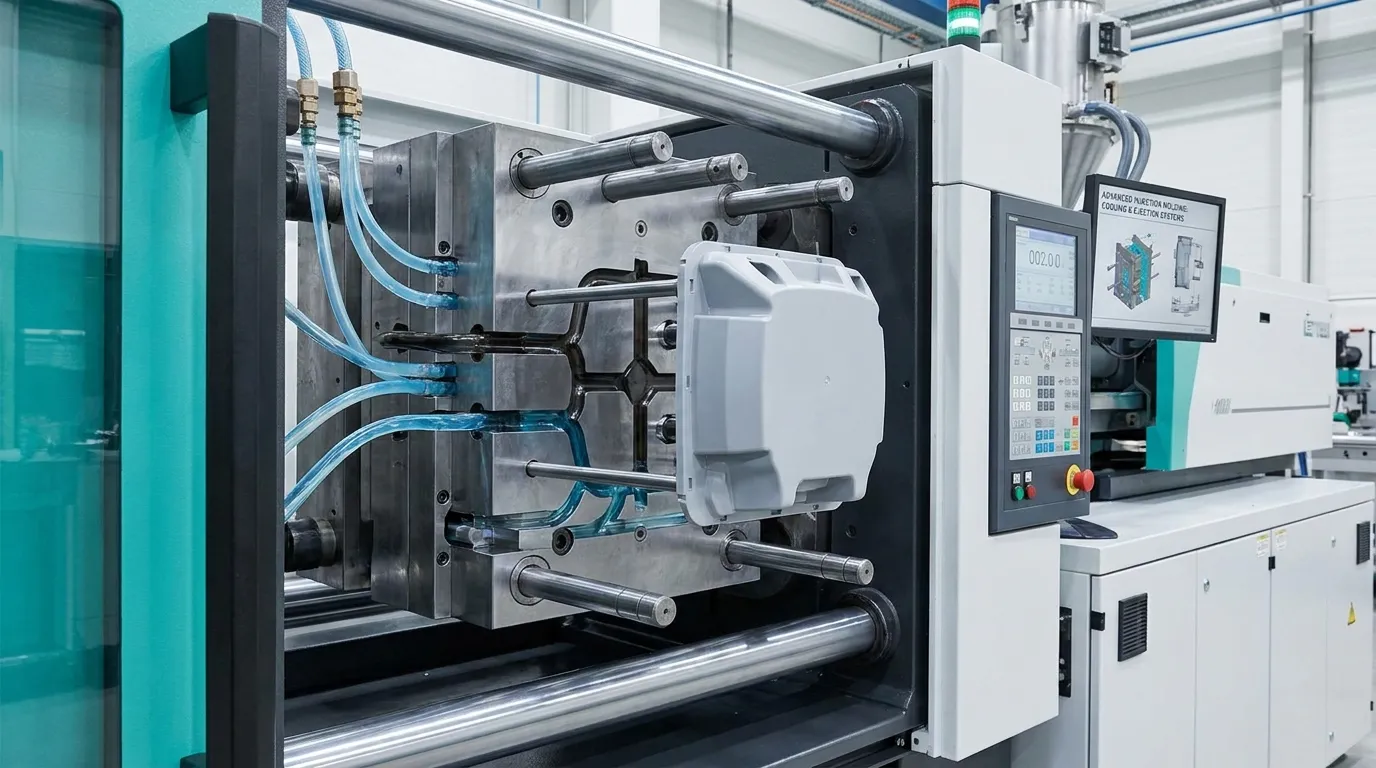
Ejection systems push cooled plastic parts out of the mold after solidification. Incorrect ejector placement can leave marks, crack parts, or create deformation during release.
Après refroidissement, the mold opens and the ejection system pushes the finished part away from the core. Most molds use ejector pins, ejector sleeves, or stripper plates depending on part geometry and surface requirements.
Le Pièces du système d’éjection guide provides additional detail about common ejection hardware used in production molds.
A standard ejection sequence usually follows these steps:
- The mold opens after cooling.
- Ejector plates move forward.
- Ejector pins contact the molded part.
- The part separates from the core.
- The ejector system retracts before the next cycle.
Different parts require different ejection strategies. Thin-wall parts often need carefully distributed ejector pins to avoid deformation. Cosmetic housings may use sleeves or stripper systems to reduce visible marks.
Problèmes courants d’éjection
| Problème | Cause probable | Résultat |
|---|---|---|
| Marques d’épingles | Pression excessive de l’éjection | Défauts esthétiques |
| Blocage des pièces | Mauvais angle de tirage | Cycle interruption |
| Fissures | Force d’éjection inégale | Pièces de ferraille |
| Déformation | Synchronisation de l’éjection à chaud | Instabilité dimensionnelle |
Replacing worn ejector pins without inspecting alignment components can waste time and money. Ejection problems sometimes start with mold misalignment, not the pins themselves.
A medical electronics housing illustrates this well. Poor ejector placement near cosmetic surfaces can leave visible witness marks, even when molding conditions stay within normal production ranges.
What do runners, gates, and cooling channels do?
Runners and gates direct molten plastic into the mold cavity, while cooling channels remove heat for stable cycle times. Poor flow or cooling design often causes short shots, warping, or sink marks.
The runner system moves molten resin from the injection unit into the cavity. Gates control how resin enters the part itself. Cooling channels then remove heat so the molded component solidifies evenly before ejection.
Selon le Entrée Wikipédia sur le moulage par injection, cooling systems strongly influence cycle time and dimensional consistency during production.
| Système | Poste principal | Problème commun |
|---|---|---|
| Coureur | Fait passer la résine dans le moule | Déséquilibre d’écoulement |
| Gate | Contrôle l’entrée de la cavité | Gel des portes |
| Canal de refroidissement | Élimine la chaleur | Refroidissement inégal |
| Vent | Libère de l’air piégé | Marques de brûlure |
Cooling design becomes especially important in high-cavitation molds. A consumer electronics mold producing multiple thin-wall housings may require upgraded cooling channels to maintain stable cycle times across every cavity.
Pourquoi la ventilation est-elle importante dans les moules d’injection
Vents allow trapped air to escape as molten resin fills the cavity. Without proper venting, compressed air can create burn marks, short shots, or incomplete filling.
Le Guide de dépannage Elastron notes that poor venting often contributes to filling defects and trapped gas problems during molding cycles.
Complex custom runner systems are not always necessary. Standardized runner layouts often simplify maintenance and reduce downtime for many production programs, especially when part geometry remains relatively simple.
Which injection mold parts wear out the fastest?
Goupilles éjecteurs, gates, Silents, and high-friction inserts usually wear out first because they experience constant movement, Pression, and heat exposure during molding cycles.
Moving and high-contact components naturally wear faster than static mold plates. Volume de production, Abrasivité de la résine, and maintenance practices all affect how quickly this happens.
Le Composants d’usure du moule section helps production teams identify common replacement areas before failures disrupt production.
Liste de contrôle des composants de moule à forte usure
| Composant | Pourquoi il s’use | Symptôme courant |
|---|---|---|
| Goupilles éjecteurs | Mouvement glissant constant | Marques de collage ou de broches |
| Silents guides | Contact d’alignement répété | Flashing |
| Portes | Vitesse élevée de résine | Incohérence de remplissage |
| Inserts | Friction et chaleur | Dérive dimensionnelle |
Le FAQ sur le moulage par injection ESCATEC explains that mold lifespan depends heavily on steel quality and operating conditions.
A buyer choosing between hardened steel ejector pins and untreated components should consider production volume carefully. Lower-cost untreated pins may work for short runs, but hardened components usually last much longer in continuous manufacturing environments.
Interchangeable inserts also wear differently depending on resin type. Glass-filled materials often accelerate abrasion on cavity inserts compared to standard resins.
What should buyers check before sourcing mold components?
Buyers should verify tolerance capability, Qualité acier, Qualité du traitement thermique, Finition de surface, and supplier delivery performance before ordering mold components for production tooling.
Mold components directly affect production reliability, so sourcing decisions should focus on consistency instead of price alone. Poorly machined or untreated components can create repeat maintenance issues that cost far more than the original savings.
Fabricants à la recherche de Composants de moule standards should compare material specifications, machining precision, and lead-time stability before placing production orders.
Liste de contrôle pour les acheteurs de composants de moisissure
- Confirmez les spécifications de qualité et de dureté de l’acier
- Vérifier la capacité de tolérance pour les pièces de précision
- Consultez la documentation du procédé de traitement thermique
- Vérifier les exigences de finition de surface
- Comparez les délais de remplacement
- Déterminez si les pièces sont standard ou personnalisées
- Évaluer la cohérence des fournisseurs sur les commandes répétées
Custom mold components are not always necessary. Standardized parts often simplify future maintenance because replacements remain easier to source and install.
Par exemple, a consumer electronics supplier using interchangeable cavity inserts can support multiple product versions without building entirely new molds. This lowers tooling costs and shortens revision lead times during product updates.
How do mold component failures affect production quality?
Mold component failures directly affect dimensional consistency, Qualité de surface, et stabilité de production. Many common molding defects trace back to worn or poorly maintained tooling parts instead of machine settings alone.
Le Pièces de moule de précision resource explains how tooling accuracy supports repeatable molding performance across long production runs.
Matrice de dépannage des défauts de moulage
| Défaut | Composant probablement défaillant | Cause commune | Inspection recommandée |
|---|---|---|---|
| Flashing | Silents guides | Désalignement du moule | Vérifier l’usure de l’alignement |
| Coup court | Porte ou évent | Écoulement restreint | Inspecter l’état de la porte |
| Marques de brûlure | Système de ventilation | Gaz piégé | Nettoyez les conduits d’aération |
| Collage | Système d’éjection | Mauvaise force de libération | Inspecter le mouvement de l’éjection |
| Déformation | Canaux de refroidissement | Température inégale | Vérifiez le débit de refroidissement |
Many processors adjust injection pressure first when flashing appears. That approach does not always solve the root issue. If guide systems are worn, the mold may continue leaking resin even with lower processing pressure.
Cooling problems create similar confusion. Uneven cooling channels often cause warping that operators mistakenly blame on material shrinkage or cycle timing. Inspecting the cooling layout usually reveals the real problem faster.
Que faire ensuite
Understanding injection molding mold parts helps manufacturers make better tooling decisions before problems appear on the production floor. The core, cavity, guide system, cooling channels, and ejector components all affect mold life and part quality in different ways.
If you're evaluating tooling suppliers or replacing worn mold components, focus on precision, material quality, and long-term repeatability instead of upfront cost alone. Standardized components can simplify maintenance, but high-cycle molds may still require upgraded materials and tighter tolerances for stable production over time.
Questions fréquemment posées
What are the components of an injection mold?
Injection molds contain several functional component groups. These usually include the core, cavity, Système d’éjection, Goupilles guides, Silents, runners, gates, cooling channels, and venting features that support molding, Alignement, and part release.
What is the core and cavity in injection molding?
The cavity and core are the primary forming components inside the mold. The cavity creates the outside shape of the part, while the core forms internal geometry and hollow sections during molding.
What do ejector pins do in injection molding?
Ejector pins safely remove molded parts from the cavity after cooling. Proper pin placement helps prevent sticking, craquelement, and visible surface marks during the ejection stage.
Which mold components wear out fastest?
High-friction and moving components usually wear out first. Goupilles éjecteurs, Silents guides, inserts, and gates experience repeated heat, Pression, and motion during production cycles.
What causes flashing in injection molds?
Flashing happens when molten plastic escapes between mold surfaces. Worn alignment components, damaged guide bushings, or poor mold closure often allow resin leakage at the parting line.
How long do injection mold components last?
Mold component lifespan depends on steel quality, resin type, maintenance practices, et volume de production. Hardened steel components generally last longer in high-cycle manufacturing environments.
Partager:



Écrit par Sunshine
Au soleil, Nous sommes un fabricant et fournisseur professionnel de composants de moule de précision, proposant une large gamme de produits pour les applications de stampage et de moulage par injection. Notre objectif principal est le poinçage des coins, Goupilles et manchons d’éjection, et poteaux guides et bagues. Avec un usinage CNC avancé, Contrôle qualité strict, et de fortes capacités de production, Nous garantissons une fiabilité, Pièces de haute précision, ainsi que des composants standards en stock pour un approvisionnement mondial rapide et efficace.
ACTUALITÉS
OBTENIR UN SERVICE
Avec des pièces de qualité adaptées à tous les budgets et un personnel accueillant formé pour rendre votre visite informative et sans tracas.
