



Sélection du fabricant de la goupille de limite de moulage: Liste de contrôle des capacités
Mold limit pin manufacturer selection should begin with the part’s function and drawing—not the supplier’s price, factory age, equipment list, or certification logos. A capable supplier must be able to produce the required geometry, control the specified material and hardness, measure the critical characteristics, document conformity, and repeat the approved result in later orders.
La première décision concerne la possibilité pour l’application d’utiliser des stocks Moulage des pièces standard (déduit) or requires a custom limit pin made from a drawing or sample. Standard and custom parts need different levels of supplier qualification, but neither should be approved on marketing claims alone.
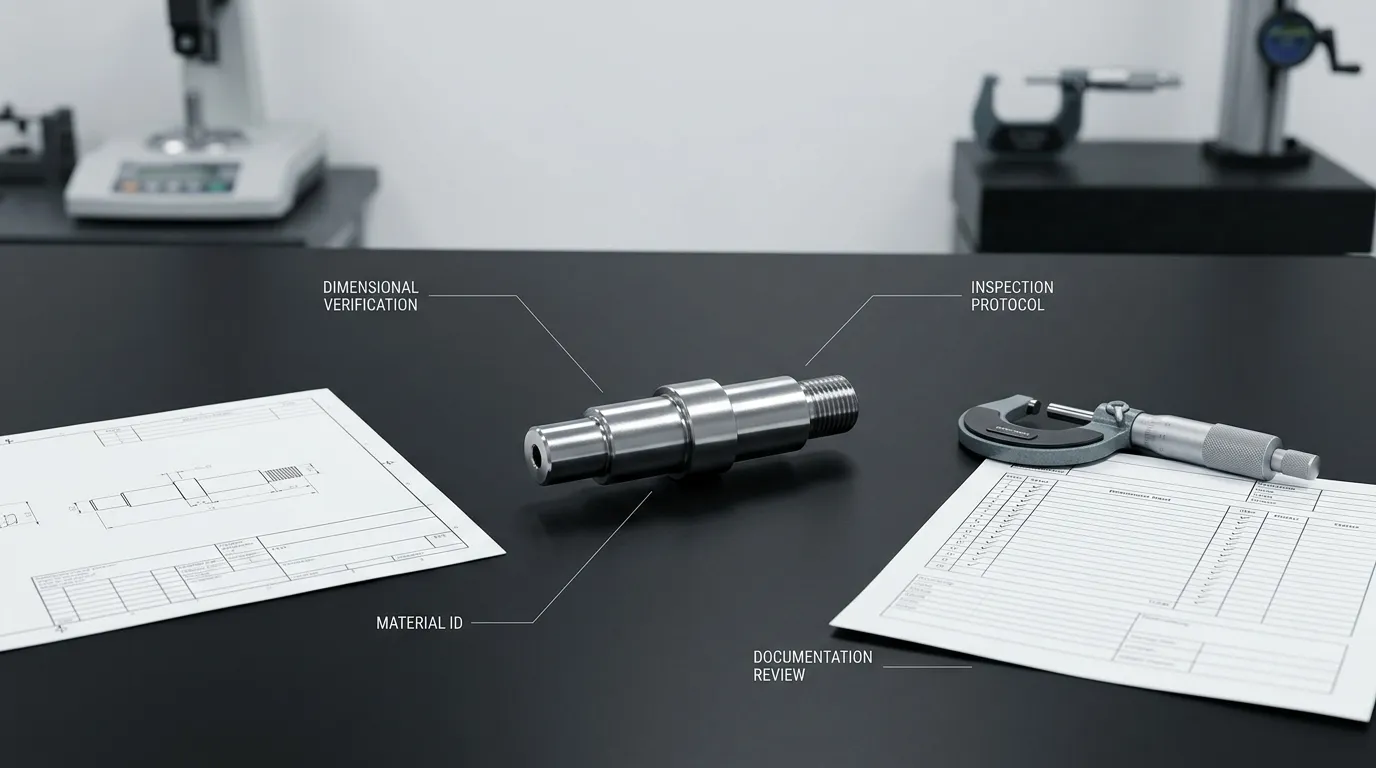
Définissez l’exigence de goupille de limite avant de comparer les fabricants
A manufacturer cannot confirm capability until the buyer defines what the limit pin must do. The same general part name may refer to components used to stop movement, limit a stroke, retain an assembly, or support a positioning function. Each use creates different critical dimensions and risks.
Start by confirming:
- what movement the pin controls;
- where the load acts;
- whether the pin receives repeated impact;
- how it seats or mounts;
- whether it has a shoulder, Tête, step, Fil, Chanfreinage, or radius;
- which dimensions affect the final stopping position;
- whether the part is for a new mold, a replacement, or a modified mechanism;
- which characteristics are mandatory for function and interchangeability.
This distinction also prevents confusion between limit pins and other cylindrical mold components. Goupilles guides, Goupilles éjecteurs, return pins, dowels, and core pins may look similar, but their operating conditions and acceptance requirements can be different. Broader alignment, Dégagement, and wear considerations are covered separately in the guide to Broches et bagues de moulage.
Confirmez ce que la broche contrôle réellement
The supplier should not be asked to quote from a part name alone. A drawing, assembly view, physical sample, or clear application description should show the pin’s intended function.
Par exemple, a dimension controlling the mold’s stopping position may need closer attention than a non-functional relief feature. A threaded section may affect retention, while a shoulder face may determine seating. If impact occurs at one end, the material condition, heat-treatment route, end geometry, and inspection priorities may also change.
The buyer should identify these critical-to-quality characteristics before sending the RFQ. Sinon, the supplier may quote a technically manufacturable part that does not address the actual functional risk.
Décidez si l’exigence est standard ou personnalisée
| Parcours d’approvisionnement | Approprié quand | Orientation de la qualification |
|---|---|---|
| Goupille de limite standard ou stockée | The supplier’s published dimensions, Matériel, Dureté, and geometry match the requirement | Confirm the exact catalog specification, stock status, Traçabilité, et la cohérence des remplacements |
| Broche standard modifiée | Une pièce de base standard nécessite un usinage limité ou des modifications de caractéristiques | Confirm which original characteristics remain controlled and how modification affects hardness, Fin, or geometry |
| Goupille de limite entièrement personnalisée | The drawing specifies non-standard dimensions, Tolérances, Matériel, Dureté, Fils, Épaules, or finish | Conduct drawing review, process review, Approbation d’exemple, dimensional verification, and repeat-order control |
A stocked part can reduce qualification work only when its documented specification matches the application. A custom part needs stronger drawing control because the approved dimensions and process route become the basis for future orders.
Préparer un dossier RFQ complet à broche de limite
A vague RFQ produces vague capability claims and quotations that are difficult to compare. The manufacturer should receive enough information to review feasibility, choose a suitable process route, identify inspection requirements, and disclose any exceptions.
A useful RFQ package should include:
Informations techniques
- revision-controlled 2D drawing;
- 3D CAD model when the geometry is difficult to interpret from the drawing;
- nominal dimensions and tolerances;
- datum references and geometric controls where functionally necessary;
- material grade and required condition;
- hardness or heat-treatment requirement;
- surface-texture requirement where relevant;
- thread standard, Taille, Classe, depth, and inspection requirement;
- coating or surface-treatment requirement, if applicable;
- approved reference sample when a drawing is incomplete.
Informations sur les commandes
- prototype or sample quantity;
- Quantité de production;
- expected repeat-order pattern;
- annual or forecast demand where available;
- required delivery destination;
- preferred shipping terms;
- required packaging and identification.
Informations sur la qualité
- dimensions requiring actual measured values;
- material-document requirements;
- heat-treatment-document requirements;
- sample or first-article expectations;
- required conformity documents;
- traceability requirements;
- treatment of deviations or substitutions;
- record-retention expectations.
The drawing should remain the controlling technical document. Les principes dans ASME Y14.5 support clear communication of dimensions, Tolérances, datums, and geometric relationships. The supplier should not be expected to infer missing functional requirements from a model or sample alone.
SunshinePro describes a workflow that begins with consultation and drawing submission, followed by review and quotation. Son mold limit pin product page can provide initial product context, but the buyer’s released drawing and agreed quotation should define a custom order.
Vérifiez les capacités de fabrication qui influencent la conformité des broches de limite
The correct manufacturing capability depends on the pin’s geometry and specification. A long equipment list is less useful than a clear explanation of how each critical feature will be produced, finished, and inspected.
The supplier should be able to connect the drawing to a realistic process sequence.
| Exigence de broche de limite | Capacité à vérifier | Preuves à demander |
| Diamètre extérieur contrôlé | Turning and, where required, final precision grinding | Explication des procédés et résultats dimensionnels |
| Géométrie à échelons ou épauliers | Stable turning, setup control, and feature relationship control | Exemple comparable ou rapport de premier article |
| Fonctionnalité filetée | Méthode appropriée de production et d’inspection du filetage | Confirmation de la spécification du thread et résultat de l’inspection |
| Dureté spécifiée | Voie de traitement thermique contrôlé et essais de dureté | Dossier de traitement et résultats de dureté lorsque nécessaire |
| Relations géométriques serrées | Suitable workholding, machining sequence, and measurement method | Plan d’inspection spécifique au dessin |
| Texture de surface contrôlée | Procédé de finition approprié et mesure de profil lorsque spécifié | Résultat et méthode texture de surface |
| Interchangeabilité en ordre de répétition | Revision control, Cohérence des processus, and retained approval records | Accord de dessin approuvé et de contrôle des changements |
Adapter la géométrie au processus de production
A simple cylindrical pin may need turning followed by grinding. A stepped, shouldered, or threaded part may require several setups and a defined sequence to maintain relationships between features.
Questions for the manufacturer should include:
- Which features will be turned, ground, threaded, or finished by another method?
- Is the final diameter established before or after heat treatment?
- How will shoulders and end faces be held relative to the main diameter?
- How will thread concentricity or alignment be checked when it affects assembly?
- Will the production sample use the same process route planned for repeat orders?
- Which dimensions are expected to change during heat treatment?
- How much finishing allowance is retained for final grinding?
The answers should relate directly to the drawing. Claims such as “high precision,” “advanced machining,” or “tight tolerance capability” are not enough without a process explanation and inspection evidence.
Verify Material, Traitement thermique, and Grinding Control
Matériel, Traitement thermique, and final grinding are connected. The material grade affects machinability and the available treatment route. Heat treatment can change hardness but may also introduce distortion. Final grinding may then be required to restore the specified diameter, geometric condition, or surface.
The supplier should confirm:
- the exact material designation;
- how incoming material is identified;
- whether a material certificate is available when required;
- the specified heat-treatment condition;
- the required hardness scale and test location;
- whether heat treatment is internal or subcontracted;
- how treatment batches are linked to finished parts;
- when final grinding occurs;
- how grinding burn, Dérive dimensionnelle, or surface damage is controlled;
- how the finished condition is verified.
SunshinePro’s product page lists S45C for its displayed mold limit pin and describes outer-diameter precision grinding and vacuum heat treatment. Those statements may support an initial capability discussion, but they do not establish that the same material, Dureté, or process is suitable for every custom application.
Where Rockwell hardness is specified, the test method should be appropriate to the material, Épaisseur, surface, and required scale. ISO 6508-1 provides the standardized method for Rockwell hardness testing of metallic materials.
Broader considerations involving steel, Fin, Tolérance, and quality inspection are addressed in the guide to Pièces de moule de précision.
Identifier quels processus critiques sont externalisés
Outsourcing is not automatically a disqualification. The risk comes from undisclosed or poorly controlled outsourcing.
Ask the prospective supplier:
- Which operations are performed at its own facility?
- Which operations are subcontracted?
- How are subcontractors approved?
- How are material and heat-treatment records linked to the finished batch?
- Who is responsible for final inspection?
- Will the buyer be notified before a critical process or subcontractor changes?
- What happens if the external processor causes a delay or nonconformance?
A supplier that controls an approved heat-treatment source and accepts full responsibility for conformity may present less risk than a supplier that claims everything is internal but cannot provide clear records.
Verify Measurement Capability, Not Just Claimed Tolerances
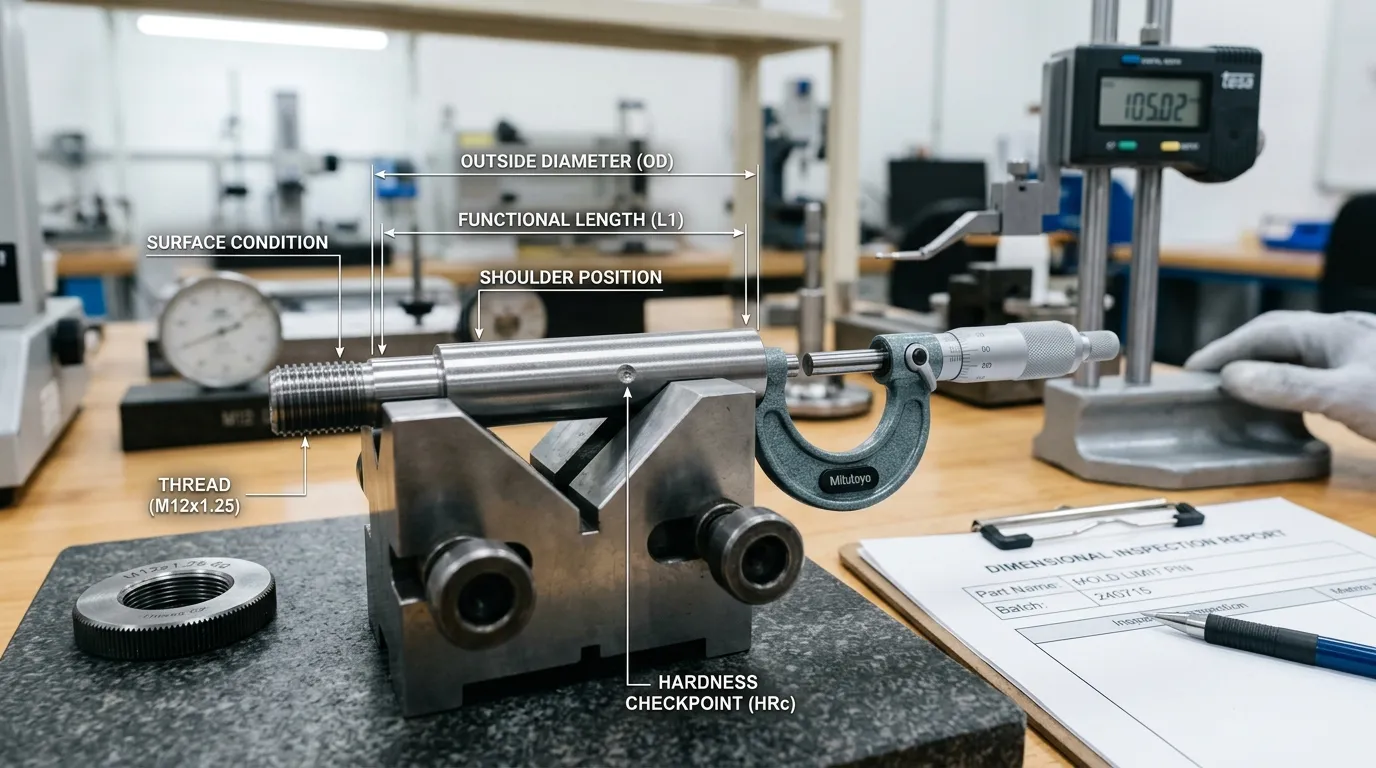
Manufacturing a dimension and measuring it reliably are separate capabilities. A supplier may say it can hold a tolerance, but the buyer still needs to know how that characteristic will be checked.
The measurement method should suit the feature, Tolérance, accessibility, and required confidence.
| Caractéristiques | Méthode d’inspection possible | Point de vérification de l’acheteur |
| Diamètre extérieur accessible | Micromètre ou un autre instrument dimensionnel approprié | Range, resolution, calibration, Emplacement de mesure, and actual result |
| Longueur ou position des épaules | Height measurement, comparator, CMM, or suitable fixture | Configuration des données et répétabilité |
| Relation géométrique | CMM ou une autre méthode validée | Equipment suitability, program, fixture, and reported result |
| Thread | Thread gauge, optical method, or other suitable inspection | Standard, Classe, depth, and acceptance method |
| Dureté | Testeur de dureté approprié | Échelle, test location, Préparation de surface, and result |
| Texture de surface | Instrument de texture de surface basé sur le profil | Paramètre, evaluation conditions, direction, and result |
The table does not prescribe one instrument for every supplier. A micrometer may be more appropriate than a CMM for an accessible external diameter, while a CMM or comparator may be useful for geometric relationships or profile features. The method should be selected from the actual drawing requirement.
A useful report should identify:
- the drawing characteristic;
- nominal value or specification;
- tolerance or acceptance limit;
- actual measured result;
- inspection status;
- measurement method or instrument where required;
- sample or batch identification;
- Révision du dessin.
ASME Y14.45 establishes practices for reporting measurement data associated with dimensional specifications. ISO 10012 addresses measurement-management systems and the control needed to support reliable measurement results.
SunshinePro states that its workflow includes initial material inspection, Inspection en cours de processus, et inspection finale. Buyers should still confirm which characteristics are checked, which instruments are used, what records are supplied, and whether actual measured values are available for their order.
Demandez des preuves avant de présélectionner le fabricant
A supplier should be evaluated on evidence that matches the project risk. Not every order needs the same document package, but critical custom parts require more than a quotation and a verbal tolerance confirmation.
Possible prequalification evidence includes:
- a redacted dimensional report for a comparable part;
- a sample material certificate;
- a heat-treatment record;
- a process-flow summary;
- identification of outsourced processes;
- calibration or measurement-control information;
- a current quality-management certificate where relevant;
- nonconformance and corrective-action procedures;
- drawing-revision and engineering-change controls;
- sample packaging and identification method.
A quality-management certificate can support confidence in the supplier’s documented system, but it does not prove that the company can produce one specific limit pin. The certificate holder, facility, scope, issuing body, and validity should be checked. Official Directives de certification ISO distinguishes certification from accreditation and explains why certificate details matter.
SunshinePro’s website refers to quality certifications, but buyers should request current documents before relying on those claims during supplier approval.
Considérez ces réponses comme des signaux d’alerte de qualification
| Réponse des fournisseurs | Risk created | Suivi approprié |
| « Nous pouvons atteindre la tolérance » sans examiner le dessin complet | Des caractéristiques ou des points de référence critiques ont pu être manqués | Demandez une méthode de révision et d’inspection du dessin marqué |
| Aucune distinction entre les spécifications de catalogue et personnalisées | La partie citée peut ne pas correspondre à la demande | Exiger une comparaison exacte des spécifications |
| Refus de divulguer des processus critiques externalisés | Risque caché de processus et de livraison | Exiger la propriété des procédés et les informations sur les sous-traitants |
| Pas de révision contrôlée du dessin | La production peut utiliser un fichier obsolète | Définir les exigences de contrôle des révisions avant de commander |
| Aucune donnée dimensionnelle d’échantillon | La capacité reste non vérifiée | Demandez un exemple ou un rapport de premier article |
| Substitution du matériau ou de la dureté sans approbation | Risque fonctionnel et d’interchangeabilité | Exiger une approbation écrite des modifications |
| Réponse vague aux parties non conformes | Des retards et des défauts répétés peuvent s’ensuivre | Demandez des procédures de confinement et d’action corrective |
| Politique de non-notification de changement | Les ordres répétés peuvent différer de la partie approuvée | Ajouter des exigences contractuelles de contrôle des modifications |
One red flag does not always require immediate rejection. It should, cependant, trigger a documented clarification or approval condition.
Qualifiez les broches de limite personnalisées grâce à des échantillons et à l’approbation du premier article
A promising quotation is not final proof of capability. For custom or function-critical limit pins, qualification should move through a controlled sample or first-article process.
- Freeze the drawing revision.
Confirm the exact drawing, model, Caractéristiques techniques, approved deviations, et exigences d’inspection. - Review the proposed process route.
Confirm material, machining sequence, Traitement thermique, Broyage, Filetage, outsourced operations, et inspection finale. - Define the sample package.
State the sample quantity and required dimensional, Matériel, Dureté, Traitement, or conformity records. - Use the intended production process.
The sample should represent the planned repeat-order method. A hand-finished prototype may not demonstrate production consistency. - Review actual measurement results.
Compare the report with every critical drawing characteristic. Do not accept a simple “passed inspection” statement when measured values were agreed. - Perform assembly or functional checks where needed.
Dimensional conformity may not reveal every seating, retention, or stopping issue. - Resolve deviations formally.
Record rework, concessions, rejected characteristics, root causes, et actions correctives. - Establish the approved baseline.
Preserve the approved drawing revision, Matériel, process route, inspection plan, Emballage, and change-notification requirements for future orders.
A formal first-article package is project-dependent. Buyers should not assume that a supplier provides FAI, PPAP, capability studies, or control plans unless those deliverables are confirmed in the quotation.
Evaluate Repeat-Order, Remplacement, and Commercial Support
Technical approval is only part of manufacturer selection. Mold limit pins may later be reordered for maintenance, repair, Remplacement, or additional molds. The supplier must therefore protect the approved configuration.
Evaluate:
- sample price and production price;
- setup charges and quotation exclusions;
- minimum order quantity;
- initial production lead time;
- repeat-order lead time;
- stocked versus made-to-order status;
- retained drawing revision;
- Matériel, Processus, or subcontractor change notification;
- batch identification and record retention;
- urgent replacement capability;
- nonconformance response;
- packaging and corrosion protection;
- thread and end-face protection;
- separation of similar part numbers;
- export packing and customs documents;
- agreed Incoterms;
- drawing confidentiality where required.
SunshinePro states that standard sizes can be supplied from stock and non-standard sizes can be customized. Its company profile also refers to flexible order quantities, technical support, and international cooperation. These points should be confirmed for the specific drawing, Quantité, Destination, and delivery requirement rather than treated as universal guarantees.
Comparez les fournisseurs avec des portes de réussite/échec avant de noter le prix
A supplier scorecard is useful only after mandatory requirements are separated from preferences. A low quotation should not compensate for an unresolved material substitution, inadequate inspection method, uncontrolled drawing revision, or missing critical process.
Use a structure such as:
| Zone d’évaluation | Exigence obligatoire | Preuves | Statut | Note à risque ou commercial |
| Critique du dessin | Toutes les exigences critiques sont reconnues | Dossier de dessin ou de révision marqué | Réussite/Échec | Exclusions de notes |
| Matériel | Grade et état exacts confirmés | Certificat ou confirmation du fournisseur | Réussite/Échec | Remplacements records |
| Itinéraire de procédé | Suitable machining, Traitement, and finishing sequence | Résumé du processus | Réussite/Échec | Identifier les étapes externalisées |
| Mesure | Méthode adaptée à toute caractéristique critique | Plan d’inspection ou rapport d’échantillon | Réussite/Échec | Notes sur les limites de rapport |
| Approbation d’exemple | Échantillons et enregistrements requis acceptés | FAI ou package d’exemple convenu | Réussite/Échec | Écarts records |
| Contrôle des modifications | Notification à l’acheteur avant des changements critiques | Police écrite ou terme de devis | Réussite/Échec | Définir la voie d’approbation |
| Support de remplacement | Conditions d’ordre de répétition comprises | Confirmation du délai d’exécution et de la conservation des records | Partition | Considérez le risque d’arrêt |
| Prix | Comparaisons de citations sur un champ d’application égal | Devis commercial complet | Partition | Inclure l’inspection et l’emballage |
Only suppliers passing the mandatory gates should proceed to commercial scoring. The final comparison can then consider communication, responsiveness, evidence quality, replacement support, Logistique, and total sourcing cost.
Total cost is broader than unit price. Refonte, delayed mold assembly, emergency freight, Temps morts, and requalification can exceed a small initial saving.
Comment SunshinePro propose des cartes à la liste de contrôle annoncée par SunshinePro
SunshinePro publishes several points relevant to an initial supplier review. Other items still need project-specific confirmation.
| Informations confirmées par le site web | Confirmez pendant la RFQ |
| Une offre de produit à goupille de limite de moisissure vivante | Adéquation exacte à la fonction et au dessin de l’acheteur |
| Tailles standard décrites comme disponibles en stock | Matériel actuel selon la spécification requise |
| Personnalisation de taille non standard | Faisabilité exacte de la géométrie et de la tolérance |
| S45C listé pour le produit affiché | Disponibilité et adéquation du matériel requis |
| Displayed diameter, Longueur, and hardness values | Contractual dimensions, Tolérances, and hardness for the custom order |
| Fonctionnalités threadées mentionnées | Norme de filetage applicable et méthode d’inspection |
| Explication du meulage de précision de dymètre extérieur | Itinéraire exact de meulage et résultat spécifique à chaque dessin |
| Traitement thermique sous vide décrit | Process ownership, specification, records, and distortion control |
| Initial, in-process, and final inspection stated | Characteristics checked, instruments used, and reports supplied |
| Processus de révision des dessins et de devis | Sample package, Délai d’exécution, MOQ, change control, and repeat-order terms |
The company’s public information can support the first screening stage. Final manufacturer approval should still be based on the released drawing, written quotation, agreed process, requested evidence, and sample results.
Liste finale de sélection du fabricant avant la RFQ
Before approving a supplier or sending a production order, Confirme ça:
- the limit pin’s function is clearly defined;
- the correct part type has been identified;
- the standard or custom sourcing path is decided;
- the drawing revision is controlled;
- Matériel, Dureté, Géométrie, Fin, and threads are specified;
- critical-to-quality characteristics are identified;
- the manufacturer has explained the process route;
- outsourced processes are disclosed;
- the inspection method suits each critical requirement;
- required reports and certificates are agreed;
- sample or first-article approval is defined;
- substitutions require written approval;
- repeat-order and change-control expectations are documented;
- packaging protects the part during international shipment;
- quotations are compared on the same technical and quality scope;
- unresolved red flags are closed before production.
Buyers with a completed drawing, sample, quantity requirement, and inspection expectations can contactez SunshinePro for a feasibility review and quotation. The request should ask for confirmation of the proposed material, manufacturing route, inspection evidence, sample plan, and commercial terms—not only a unit price.
Partager:



Écrit par Sunshine
Au soleil, Nous sommes un fabricant et fournisseur professionnel de composants de moule de précision, proposant une large gamme de produits pour les applications de stampage et de moulage par injection. Notre objectif principal est le poinçage des coins, Goupilles et manchons d’éjection, et poteaux guides et bagues. Avec un usinage CNC avancé, Contrôle qualité strict, et de fortes capacités de production, Nous garantissons une fiabilité, Pièces de haute précision, ainsi que des composants standards en stock pour un approvisionnement mondial rapide et efficace.
ACTUALITÉS
OBTENIR UN SERVICE
Avec des pièces de qualité adaptées à tous les budgets et un personnel accueillant formé pour rendre votre visite informative et sans tracas.
