



Composants de moules d’injection en plastique: Les acheteurs de pièces standard devraient le savoir
Plastic injection mold components include the core, cavité, Système de coureurs, Conduits de refroidissement, Système d’éjection, vents, and alignment parts that control part quality and mold performance. Buyers should focus on component precision, Résistance à l’usure, cooling efficiency, and maintenance accessibility because these factors directly affect mold lifespan, Temps morts, Taux de défauts, and long-term tooling cost.
A mold can look well-built from the outside and still create expensive production problems. Most tooling issues start with component quality, Alignement, Balance de refroidissement, or wear resistance. Si vous cherchez un nouveau moule, understanding how each component affects maintenance and production stability helps you avoid downtime, rejected parts, and early tooling replacement. This guide breaks down the standard parts buyers should evaluate before approving a mold build.
What are the main plastic injection mold components?
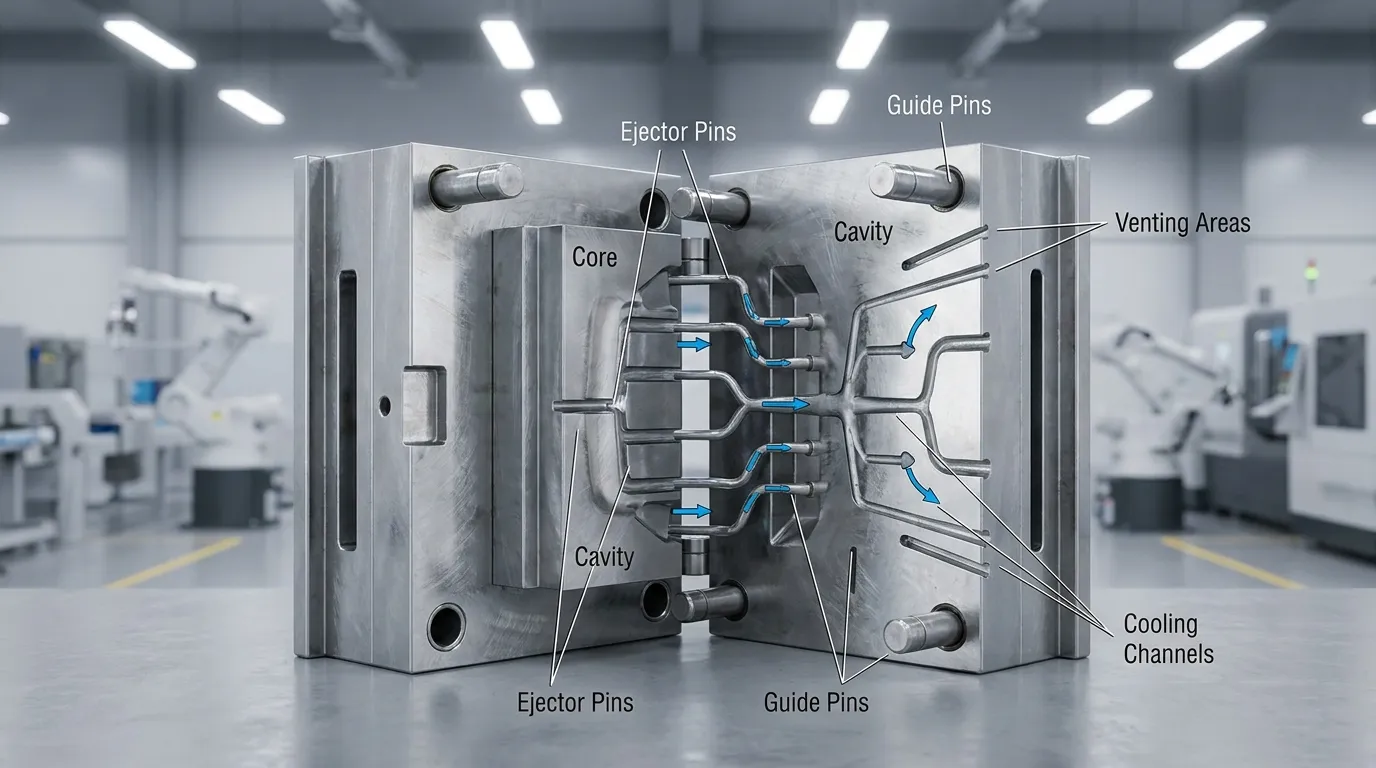
Plastic injection mold components include the mold base, Noyau et cavité, Système de coureurs, Système d’éjection, Conduits de refroidissement, vents, and alignment parts. Each component affects part quality, Temps de cycle, Fréquence de maintenance, and overall mold lifespan.
Most injection molds use the same core systems, even when the finished products are very different. The mold base supports the structure, while the core and cavity shape the plastic part itself. The runner system moves molten plastic into the cavity, and the ejector system pushes the finished part out after cooling.
Cooling channels remove heat during production. Venting systems release trapped air that could otherwise create burn marks or incomplete filling. Guide pins and bushings keep both mold halves aligned during every cycle.
If you need a broader overview of how these systems fit together, Sunshine Pro Guide complet des composants du moule explains the full mold structure and production workflow.
Composants qui façonnent la partie en plastique
The core and cavity are the most critical shaping components. Their machining accuracy directly affects dimensions, Finition de surface, et la cohérence des parties. Gates and runners also influence filling pressure and material flow.
Selon Guide des composants du moule d’injection de First Mold, these systems work together to control how material enters and forms inside the mold.
Components that control cooling, Éjection, and alignment
Cooling channels manage temperature during production. Ejector pins remove the finished part after solidification. Guide pins and bushings maintain alignment between moving mold halves.
Vous pouvez explorer plus en détail Systèmes de composants de moule if you're comparing tooling configurations across suppliers.
| Composant | Fonction principale | Préoccupation de l’acheteur |
|---|---|---|
| Noyau et cavité | Façonnez le produit | Résistance à l’usure |
| Système de coureurs | Livrez du plastique en fusion | Bilan de flux |
| Canaux de refroidissement | Retirer la chaleur | Régularité des cycles |
| Goupilles éjecteurs | Sortie des parties terminées | Fréquence d’usure |
| Goupilles guides | Maintenir l’alignement | Précision à long terme |
| Système de ventilation | Libérez de l’air piégé | Prévention des défauts |
Which mold components affect mold life and part quality the most?
Core and cavity precision, cooling efficiency, venting quality, and guide alignment have the biggest impact on mold life and part consistency. Poor-quality components increase flash, Plans courts, Usure, and unplanned maintenance.
Not every mold component deserves the same level of investment. Buyers should prioritize the systems that directly affect dimensional accuracy, heat control, and repeated mechanical movement.
The core and cavity usually see the highest pressure and repeated thermal cycling. Poor steel quality or weak machining tolerance in these areas can shorten mold life quickly. Even small alignment errors may lead to flash defects, Usure inégale, or part inconsistency.
Cooling design also has a bigger impact than many buyers expect. A mold with balanced cooling often performs better over time than one with expensive cosmetic finishes but weak thermal control. That matters in high-volume production where cycle stability affects output every day.
Décomposition des composants de moule de RapidDirect highlights how cooling, Ventilation, and alignment systems affect molding stability and defect prevention.
| Aire composante | Production Impact | Risque commun |
|---|---|---|
| Noyau et cavité | Dimensions de la pièce | Usure prématurée |
| Canaux de refroidissement | Régularité des cycles | Déformation |
| Système de ventilation | Diffusion aérienne | Marques de brûlure |
| Goupilles guides | Alignement | Défauts de flash |
| Système d’éjection | Sortie partielle | Collage ou dommage |
Cheap wear components often create more long-term downtime than buyers expect. Saving money on guide systems or ejector hardware may reduce upfront tooling cost, but recurring maintenance usually costs far more during production.
If you're evaluating higher-grade tooling systems, Sunshine Pro Pièces de moule de précision page covers common precision component configurations.
What does each major mold component actually do?
Every major mold component controls a specific production task. Some manage material flow, while others handle cooling, Alignement, or part release after molding.
Composants d’alimentation et de conduit
The runner system moves molten plastic from the injection machine into the mold cavity. Gates control how material enters the cavity and affect filling speed, Pression, et finition de surface.
Sprue bushings connect the machine nozzle to the runner system. Poor gate or runner design can create uneven filling, Air piégé, or cosmetic defects.
Refroidissement, Ventilation, and ejection components
Cooling channels remove heat from the mold after injection. Uneven cooling often causes shrinkage variation or warped parts. Venting systems release trapped gas during filling to prevent burn marks and incomplete shots.
Ejector pins push the finished part out after cooling. Weak ejector alignment can damage parts or create sticking during high-cycle production.
Guide pins and bushings keep both mold halves aligned during every cycle. Worn alignment systems commonly lead to flash defects near parting lines.
Guide des composants de moules d’injection de MoldPartner explains how these systems work together during production.
Les acheteurs comparant les agencements d’outillages peuvent consulter davantage Pièces pour moule d’injection to better understand standard component configurations.
Which injection mold components usually wear out first?
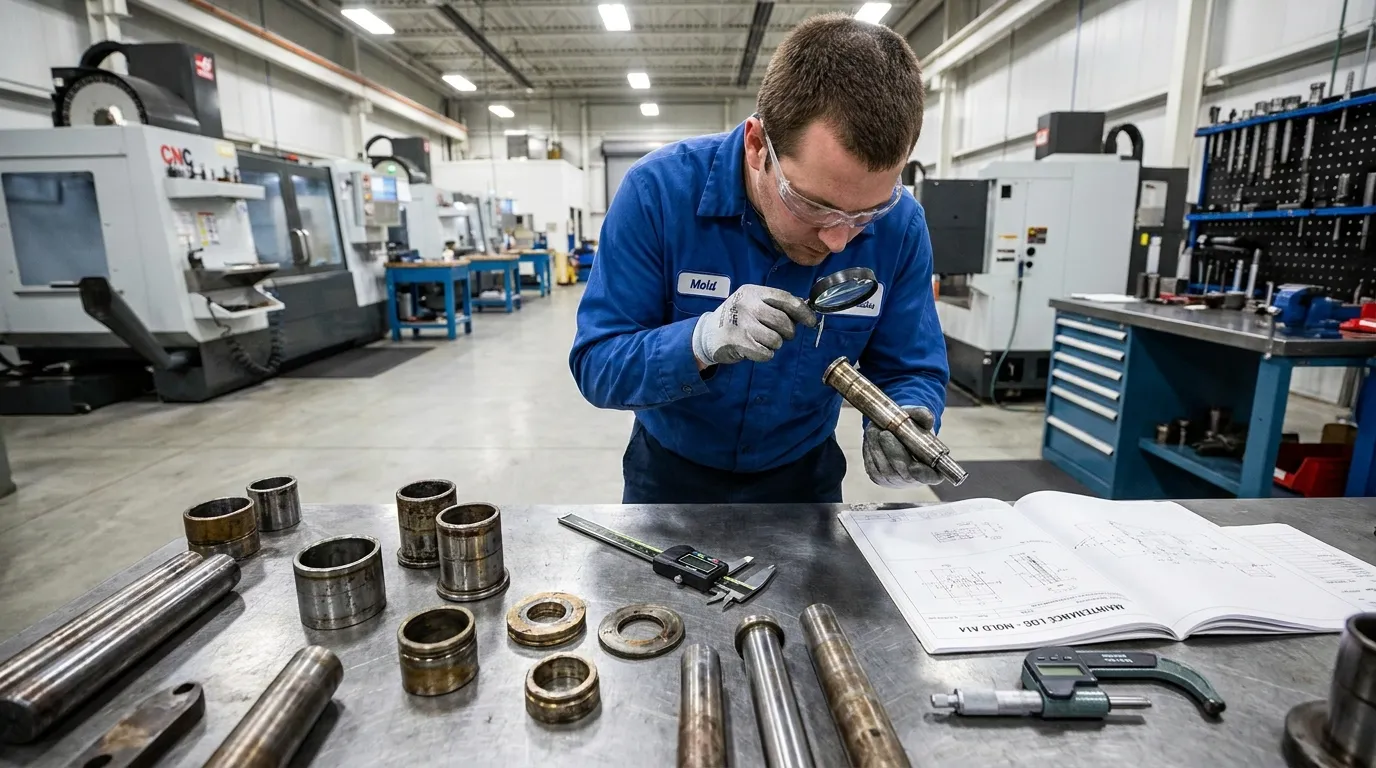
Goupilles éjecteurs, Portes, diapositives, Silents, and high-friction inserts usually wear first because they face repeated movement, Pression, and heat exposure. These components often determine maintenance frequency and unexpected production downtime.
Wear rates depend on resin type, Volume de production, and mold design. Abrasive materials such as glass-filled plastics can accelerate wear on ejector systems, Portes, and inserts much faster than standard resins.
A high-volume consumer electronics mold using abrasive resin may wear ejector pins within months if low-grade steel was selected. Dans de nombreux cas, the issue is not the mold design itself. The problem starts with material hardness and repeated friction during cycling.
Guide de moulage par injection d’Escatec notes that maintenance planning and component quality heavily influence mold longevity.
Tableau des risques d’usure des composants de moule
| Composant | Cause d’usure fréquente | Symptômes d’échec | Fréquence de remplacement | Risque d’arrêt |
|---|---|---|---|---|
| Goupilles éjecteurs | Friction et chaleur | Blocage des pièces | Haut | Moyen |
| Portes | Débit à haute pression | Remplissage flash ou inégal | Moyen | Moyen |
| Silents | Mouvements répétés d’alignement | Désalignement | Moyen | Haut |
| Glissières et inserts | Friction des mouvements latéraux | Usure de surface | Haut | Haut |
| Canaux de refroidissement | Accumulation d’échelles | Refroidissement inégal | Low | Moyen |
Low-cost inserts are not always a bad choice. They can work well for short-run tooling or prototype programs where production cycles remain limited. For long production schedules, hardened components usually provide better long-term value.
Vous pouvez comparer les courants Pièces d’usure du moule when evaluating maintenance planning and spare inventory needs.
Why do cooling and venting systems matter so much?
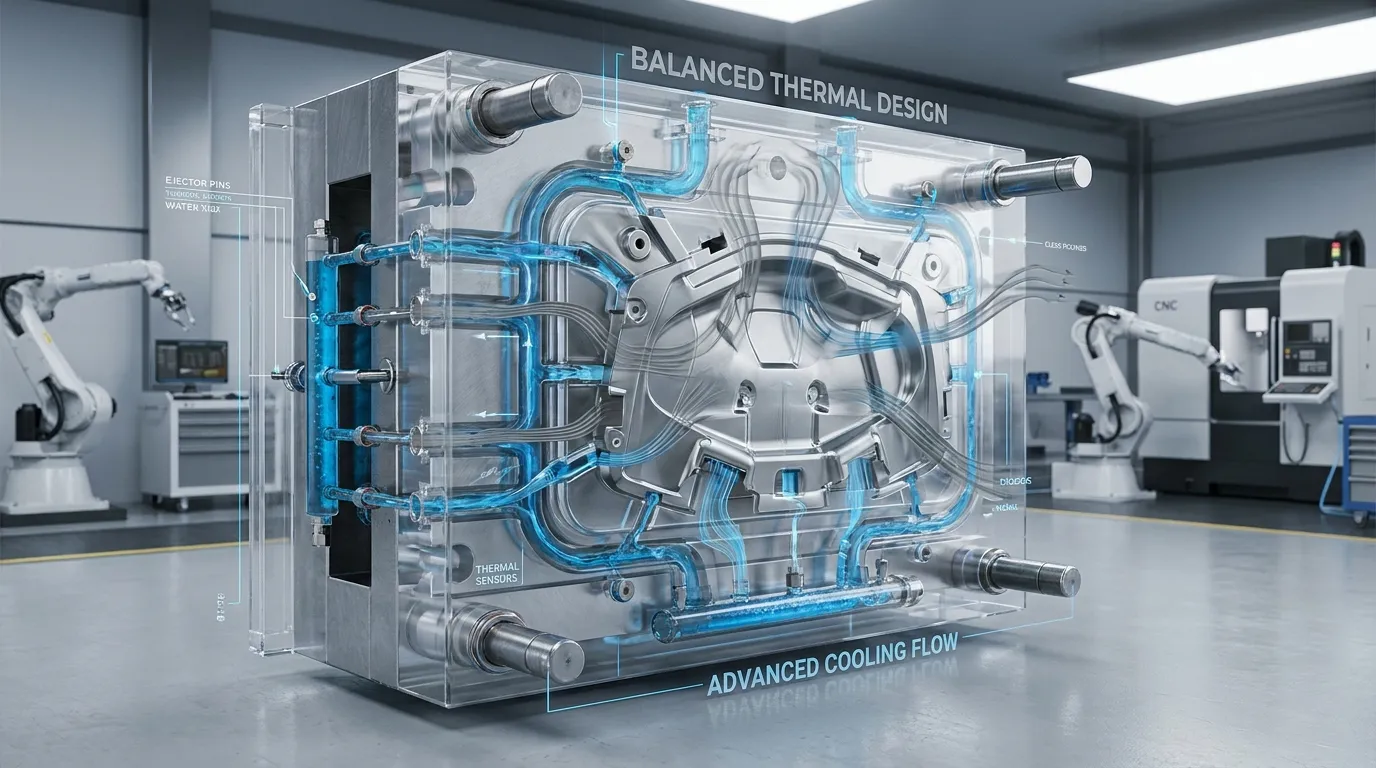
Cooling channels and venting systems directly affect cycle time, Stabilité dimensionnelle, and defect rates. Poor cooling creates warping and uneven shrinkage, while weak venting can trap air and cause burns or incomplete filling.
Cooling systems control how quickly heat leaves the mold after injection. Balanced cooling helps maintain consistent dimensions and stable production cycles. When cooling paths are uneven, one side of the part may shrink faster than the other.
That problem becomes expensive during long production runs. A medical molding supplier reduced cycle variation after redesigning cooling channels for more balanced heat removal. The mold itself did not change significantly, but cooling consistency improved part quality and reduced rejection rates.
Venting systems solve a different problem. Air trapped inside the cavity must escape during filling. Sans ventilation adéquate, pressure builds inside the mold and creates burn marks, Plans courts, or trapped gas defects.
Guide des défauts du moulage par injection d’Elastron explains how poor cooling and venting contribute to common molding defects.
- Marques de brûlure près de la fin du remblai
- Retrait inégal
- Pièces déformées
- Plans courts aléatoires
- Cycles de refroidissement plus longs
- Dimensions incohérentes
What should buyers inspect before approving mold components?
Buyers should inspect steel grade, Précision de l’usinage, Conception du refroidissement, alignment precision, and replaceable wear parts before approving a mold. Early inspection reduces future downtime, defect risk, et les coûts de réparation.
Many tooling problems are easier to prevent before production starts. Buyers should review mold drawings, Configurations de refroidissement, wear components, and maintenance access before final approval.
Steel hardness matters because it affects wear resistance and long-term dimensional stability. Surface finish quality also affects part appearance and release consistency. Poor machining tolerance can create alignment issues that only appear after thousands of cycles.
A mold producing flash defects is often traced back to worn alignment components rather than machine settings. That’s why guide systems and bushings deserve careful inspection before acceptance.
Questions que les acheteurs devraient poser aux fournisseurs
- What steel grades are used for core and cavity sections?
- Are wear inserts replaceable?
- Which components are standardized?
- How are cooling channels balanced?
- What spare parts are recommended?
- Which components are expected to wear first?
Liste de contrôle pour l’inspection des composants de moisissure
| Zone d’inspection | Que vérifier | Pourquoi c’est important |
|---|---|---|
| Dureté de l’acier | Certification des matériaux | Résistance à l’usure |
| Finition de surface | Qualité de polissage | Consistance cosmétique |
| Disposition de refroidissement | Conception de canaux équilibrés | Temps de cycle stable |
| Systèmes d’alignement | Précision de goupille et de bague | Prévention des éclairs |
| Inserts remplaçables | Accessibilité à la maintenance | Réparations plus rapides |
| Pièces détachées | Disponibilité standard des composants | Temps d’arrêt réduit |
Liste de contrôle des approvisionnements du groupe Rodon provides additional supplier evaluation questions for tooling buyers.
Pour plus d’exemples de Outillages de moulage standards, buyers can compare commonly used replaceable systems and wear components.
Are premium mold components always worth the cost?
Premium mold components are usually worth the cost for high-volume production, matériaux abrasifs, and tight-tolerance parts. Lower-cost components may work for prototype or low-volume molds with limited production cycles.
Premium components make the biggest difference when molds run continuously or process abrasive materials. Inserts durcis, Systèmes de guidage de précision, and high-grade cooling hardware usually reduce maintenance frequency in demanding production environments.
That does not mean every project needs top-tier tooling. A low-volume prototype mold with limited production cycles may never recover the added cost of premium wear systems. Dans ces cas, simpler components often make financial sense.
Comparaison d’acheteurs If-Then
| Conditions de production | Meilleure option | Raison |
|---|---|---|
| Production en grande quantité | Composants premium | Durée de vie plus longue |
| Résine abrasive | Inserts durcis | Réduction de l’usure par friction |
| Tolérances strictes | Systèmes d’alignement de précision | Meilleure régularité |
| Outils prototypes | Pièces de qualité standard | Coût initial plus bas |
| Courtes productions | Inserts moins coûteux | ROI plus rapide |
Cheap ejector and guide systems often create repeated downtime during long production runs. The upfront savings may disappear quickly once maintenance interruptions begin affecting output.
Aperçu des outillages d’Escatec discusses how tooling choices influence maintenance and long-term operating cost.
If you're comparing tooling grades, Sunshine Pro Guide des composants d’outillages can help identify where higher-spec parts matter most.
How can standardized mold components reduce downtime and sourcing delays?
Standardized mold components simplify maintenance, shorten replacement lead times, and reduce sourcing risk. Buyers using standardized systems can replace wear parts faster and minimize production interruptions during supply-chain delays.
When molds rely on custom-only hardware, repairs often take longer and cost more. Standardized guide pins, Silents, Systèmes d’éjection, and inserts are easier to source locally or through multiple suppliers.
That flexibility becomes important during customs delays or international shipping disruptions. A buyer avoided six weeks of downtime because standardized bushings and guide pins were available from a local distributor instead of requiring overseas replacement orders.
Standardization also simplifies spare inventory planning. Maintenance teams can stock fewer unique parts across multiple molds, which lowers inventory complexity and speeds up repairs.
Les acheteurs qui planifient une production à long terme devraient examiner Systèmes de moule standardisés before approving custom tooling configurations.
If you need a broader process-level overview, Sunshine Pro Guide pour moule d’injection plastique explains how tooling systems connect to production planning and mold maintenance.
Réussir la prochaine étape
Choosing the right plastic injection mold components is less about buying the most expensive mold and more about matching component quality to production reality. High-volume programs, Résines abrasives, and tight tolerances usually justify stronger wear systems and precision cooling designs. Prototype tools and short-run molds often need a different balance.
Before approving a mold, focus on cooling layout, wear components, alignment systems, and maintenance accessibility. Those details usually decide whether a mold runs reliably for years or becomes a constant repair problem.
Questions fréquemment posées
What are the main components of a plastic injection mold?
The main components include the mold base, Noyau et cavité, Système de coureurs, Système d’éjection, Conduits de refroidissement, vents, et composants guides. Each part supports molding accuracy, cooling efficiency, part release, or mold alignment.
Quels composants de moulage s’usent le plus rapidement?
Goupilles éjecteurs, Portes, Silents, diapositives, and inserts usually wear fastest because they experience repeated movement, Chaleur, and friction. These components often require the most frequent inspection and replacement.
Why are cooling channels important in injection molds?
Cooling channels control heat removal and cycle consistency during molding. Poor cooling design can increase warping, shrinkage variation, and production delays.
How long does an injection mold last?
Injection mold lifespan depends on steel quality, Abrasivité de la résine, Pratiques de maintenance, et volume de production. Well-maintained hardened steel molds can last hundreds of thousands or even millions of cycles.
What causes defects in injection molding molds?
Common mold-related defects come from poor venting, Déséquilibre de refroidissement, worn ejector systems, or alignment problems. These issues can create flash, burn marks, Plans courts, or dimensional inconsistency.
Are premium mold components necessary for every project?
Premium components are most valuable for high-volume production, Résines abrasives, and tight-tolerance applications. Lower-cost components may be acceptable for prototypes or short-run tooling.
Partager:



Écrit par Sunshine
Au soleil, Nous sommes un fabricant et fournisseur professionnel de composants de moule de précision, proposant une large gamme de produits pour les applications de stampage et de moulage par injection. Notre objectif principal est le poinçage des coins, Goupilles et manchons d’éjection, et poteaux guides et bagues. Avec un usinage CNC avancé, Contrôle qualité strict, et de fortes capacités de production, Nous garantissons une fiabilité, Pièces de haute précision, ainsi que des composants standards en stock pour un approvisionnement mondial rapide et efficace.
ACTUALITÉS
OBTENIR UN SERVICE
Avec des pièces de qualité adaptées à tous les budgets et un personnel accueillant formé pour rendre votre visite informative et sans tracas.
