



Liste de contrôle pour inspection des goupilles de perforation pour le contrôle qualité entrant et de routine
A punch pin inspection checklist should answer four questions: Is this the correct punch? Does it match the approved specification? Is it still fit for service? What action should follow the inspection?
This guide covers individual punch pins used in metal-stamping dies. Incoming QC verifies a newly supplied punch against the purchase order, Dessin, revision, et la documentation requise. Routine QC checks whether a punch remains serviceable after production use, regrinding, a collision, or another abnormal event.
Punch pins work within a larger die system. Guides, Silents, retainers, stripper components, L’Autorisation, and alignment can all influence punch condition. The broader roles of these components are covered in the Guide des composants de la puce (déduit). Tiens, the focus stays on inspecting and dispositioning the punch pin itself.
No universal tolerance, inspection interval, or wear limit applies to every punch pin. Acceptance must be based on the approved drawing, purchase specification, control plan, or another documented requirement.
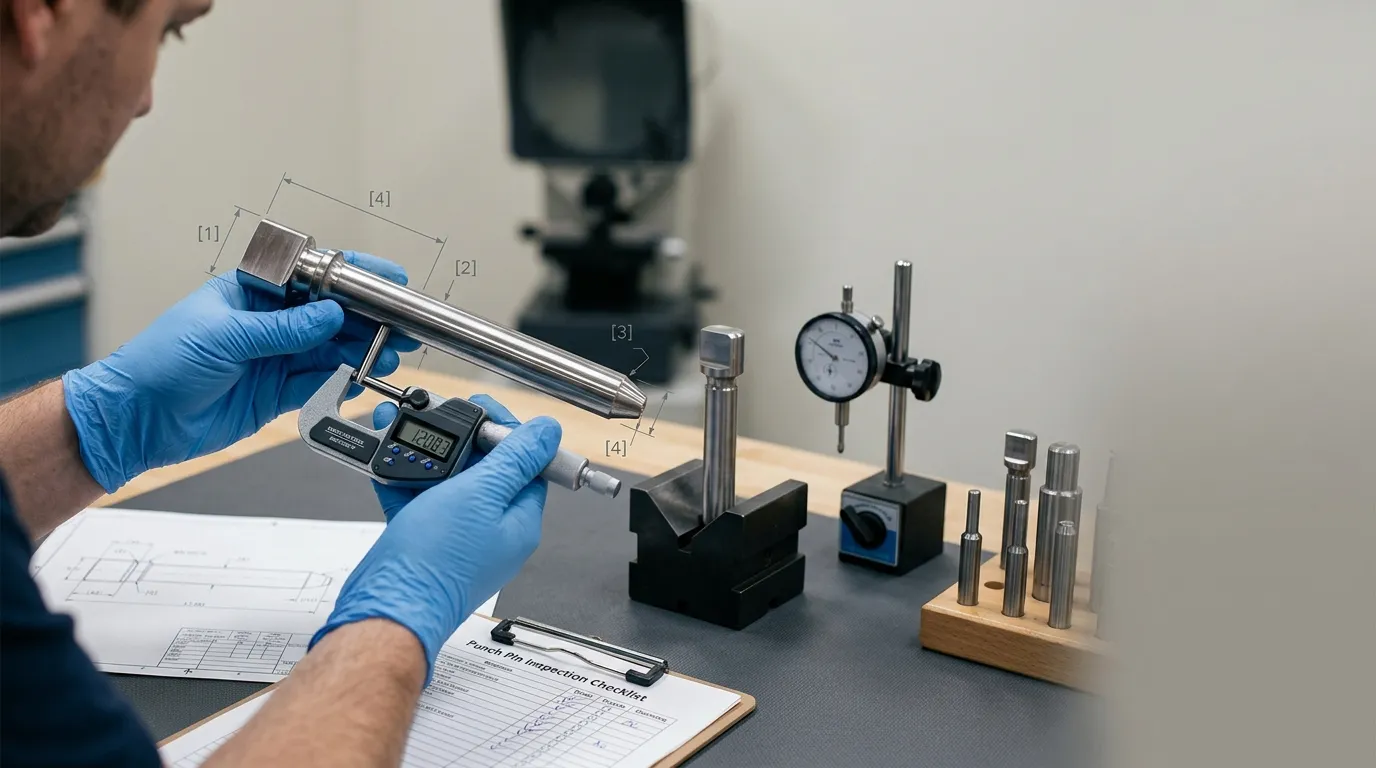
Contrôle QC entrant et QC de routine : différents risques
Incoming and routine inspection use many of the same instruments, but they answer different questions.
| Phase d’inspection | Objectif principal | Contrôles typiques | Décision principale |
|---|---|---|---|
| Contrôle qualité entrant | Confirmez que le punch fourni correspond à la commande et aux spécifications approuvées | Part identity, Révision du dessin, material or coating documents, visible damage, Dimensions, Géométrie, inspection report | Accept, hold, return, or reject |
| Contrôle qualité de routine | Confirmez qu’un poinçon usagé reste sûr et fonctionnel | Usure des bords, fissures, Irritant, Changement dimensionnel, runout, Longueur de travail, Symptômes de production, regrind history | Return to service, Moniteur, regrind, remplacer, or investigate |
| Inspection post-meulage | Confirmez que l’affûtage a restauré le tranchant sans rendre les autres caractéristiques inacceptables | Edge form, burr removal, Longueur totale, Longueur de travail, Profil, Condition de la surface | Release, rework, ou remplacer |
| Inspection post-événement | Check for hidden or visible damage after a jam, collision, misfeed, or nearby breakage | Fissures, Maîtrise, head damage, runout, Surfaces de sièges, Composants d’accouplement | Quarantine, Enquêter, Réparation, ou remplacer |
Incoming inspection should establish a reliable baseline. Recording the punch’s as-received dimensions and condition makes later wear easier to identify.
Routine inspection compares the current punch against that baseline and any approved service limits. A punch can remain within its original manufacturing tolerance yet show an abnormal wear trend. Inversement, a worn feature may still appear visually acceptable while no longer meeting the documented service requirement.
Prepare the Punch, Documents, and Measuring Equipment
Inspection should not begin with a caliper. It should begin with the correct documents, part identity, and measurement conditions.
- Confirm the inspection stage. Record whether the punch is incoming, in routine service, newly reground, or being checked after an abnormal event.
- Obtain the approved drawing. Verify the drawing number and revision before measuring anything. An accurate measurement against an obsolete revision is still an invalid inspection result.
- Review the purchase and quality requirements. Check the purchase order, control plan, approved sample, inspection-report requirement, and any requested material, traitement thermique, Dureté, or coating documentation.
- Match the punch to its records. Confirm the part number, lot or serial number, Quantité, material designation, coating designation, and any engraved identification.
- Inspect the packaging before cleaning. Record impact damage, Corrosion, broken protective packaging, loose punches, or signs that sharp edges contacted each other during transport.
- Clean the punch carefully. Remove oil, dirt, Puces, and transferred material without rounding the cutting edge or scratching a coated surface. Residue on a diameter or seating face can affect the measurement.
- Stabilize the part when tolerances are tight. A punch arriving from a hot production area, cold warehouse, or vehicle may need time to reach the inspection environment. Temperature differences can affect dimensional results.
- Verify the measuring equipment. Check instrument identification, calibration status, measuring range, Résolution, Condition de contact, and cleanliness. Confirm that any V-block, center, Calendrier, or surface plate is also clean and suitable for the feature.
SunshinePro states that non-standard mold parts can be processed from customer drawings, while its punch-pin page lists diameter, Longueur, Style de tête, Qualité des matériaux, and coating as customizable characteristics. Those fields should therefore be treated as drawing- and order-specific requirements rather than assumed product defaults.
Résoudre les spécifications en conflit ou manquantes avant la mesure
Do not select a tolerance from memory, an old inspection sheet, or a generic catalog.
Place the punch on hold when:
- the drawing revision does not match the purchase order;
- the inspection report refers to another part or lot;
- the drawing and purchase specification contain conflicting limits;
- the material or coating designation is missing;
- the required datum or measurement method is unclear;
- an approved deviation is mentioned but not supplied.
Obtain written clarification from the responsible engineer, customer, or supplier before assigning a pass or fail result. The controlling-document hierarchy should follow the customer’s quality system or contract rather than an informal assumption.
Inspectez chaque caractéristique de poinçon pour détecter des dommages visibles
Visual inspection is the fastest way to find obvious defects, but it should follow a consistent feature-by-feature sequence.
Use clean lighting and suitable magnification. Rotate the punch and inspect the complete circumference rather than viewing only one side.
| Zone d’inspection | Conditions à vérifier | Signification possible | Action suivante typique |
| Tranchant et embout | Ébréchage, fissures, Arrondissement des arêtes, meules, Déformation, micro | Loss of cutting quality, local overload, Impact, Usure, adhesive material transfer | Mesure, quarantine, regrind, ou remplacer |
| Tige ou corps | Scoring, Irritant, wear bands, Corrosion, Fretting, Matériel transféré | Poor guidance, Friction, Désalignement, lubrication problem, Ajustement incorrect | Clean, measure diameter/runout, inspect mating parts |
| Tête et épaule | Apparition en champignons, peening, fissures, uneven seating marks, Déformation | Surcharge, incorrect seating, retainer problem, inadequate support | Mettre en quarantaine et inspecter l’état de contention ou de la place |
| Rayons de transition | Fissures, grinding marks, abrupt surface changes | Concentration de contrainte, Dégâts de grinding, fatigue initiation | Magnify, escalate, ou remplacer |
| Surface revêtue | Peeling, Écaillage, rayures, discoloration, Substrat exposé | Coating damage, Friction, Impact, Corrosion, Usure | Record location, assess function, seek engineering review |
| Marques d’identification | Missing or illegible part, lot, or serial information | Perte de traçabilité ou risque de mélange des révisions | Attendez jusqu’à confirmation de l’identité |
A small chip at the cutting edge is not equivalent to a superficial scratch on a non-working surface. The inspection record should state the defect location, approximate extent, and whether it affects a functional feature.
Fissures, Déformation sévère, or a damaged retention head generally justify immediate quarantine. Galling, micro, or one-sided scoring may require inspection of the die system as well as the punch. Detailed causes of cracking and catastrophic failure belong in the guide to Cassure de la poinçon dans les matrices d’emboutissage.
Ce que l’inspection visuelle ne peut pas confirmer
Visual inspection cannot reliably establish:
- exact body or tip diameter;
- overall or working length;
- Droiture;
- runout, Concentricité, or coaxiality;
- shaped-tip profile;
- numerical surface roughness;
- Qualité des matériaux;
- heat-treatment conformity;
- Dureté;
- coating identity.
A punch may look undamaged but still be dimensionally out of tolerance. Qualité des matériaux, Dureté, and coating conformity may require traceable documentation or a specified test method.
Mesurer les dimensions et la géométrie qui contrôlent l’ajustement et la fonction
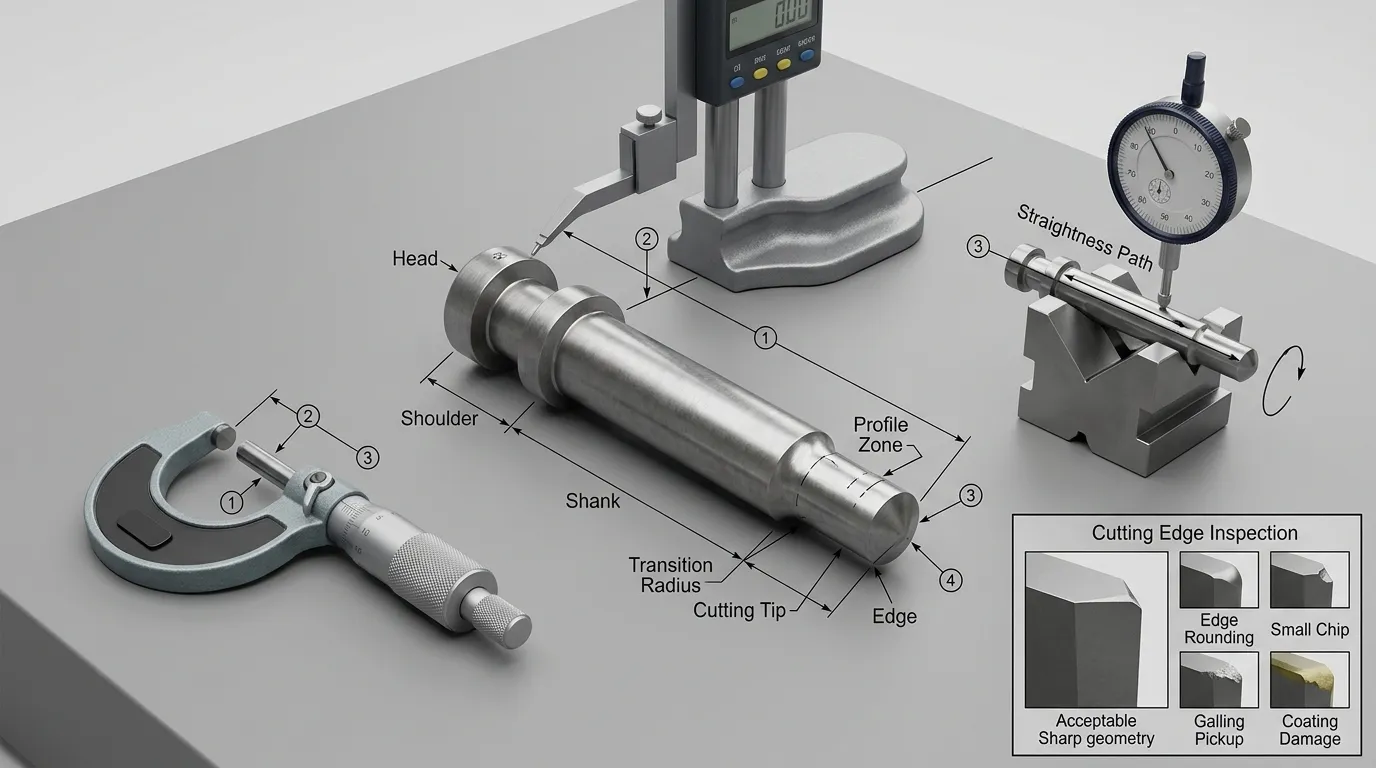
The approved drawing determines which dimensions and geometric controls must be inspected. Not every punch requires every measurement.
| Caractéristiques | Pourquoi cela compte | Méthode de mesure possible | Important limitation | Source d’acceptation |
| Diamètre du corps ou de la tige | Affects guidance, Ajusté, Rétention, et alignement | Outside micrometer; suitable limit gauge | La localisation du contact et la réduction progressive doivent être prises en compte | Spécification de dessin ou d’ajustement |
| Diamètre de la pointe | Affecte la taille des caractéristiques percées et la relation entre les dés de poinçage et la dé | Micromètre, specialized gauge, optical system | De petites pointes ou des pointes délicates peuvent ne pas convenir aux lentilles standard | Dessin |
| Profil de pointe façonné | Contrôle les trous non ronds ou la géométrie formée | Optical comparator, vision system, CMM | Nécessite un alignement correct des références et une interprétation du profil | Dessin avec l’exigence de profil |
| Longueur totale | Supports identification, installation, and regrind tracking | Height gauge, micrometer, Comparateur, dedicated fixture | Les faces des sièges doivent être propres et régulièrement référencées | Dessin |
| Longueur de travail ou projection | Influence la position opérationnelle et la pénétration | Height gauge, Comparateur, dedicated inspection fixture | Definition must match the drawing; do not borrow tablet-tooling terminology | Conception ou spécification de configuration |
| Diamètre et épaisseur de la tête | Affecte la rétention et la disposition des assises | Micromètre, caliper for screening, Comparateur | Les meules ou le peening peuvent déformer le contact | Dessin |
| Position des épaules | Influences sur les sièges et la projection assemblée | Height gauge, Comparateur, CMM | La configuration des références doit reproduire l’exigence de dessin | Dessin |
| Droiture | Détecte la courbure ou la déviation d’axe | Indicator with suitable support, CMM, dedicated fixture | La méthode de support et le choix du datum influencent le résultat | Tirage ou limite de service approuvée |
| Circulaire ou totalisation | Montre la variation de rotation par rapport à un axe de référence | Indicator with centers or V-block; CMM | « Runout » doit correspondre exactement au contrôle de tirage | Dessin |
| Concentricité ou coaxialité | Évalue la relation entre axes ou caractéristiques | CMM ou méthode spécialisée approuvée | Ne remplacez pas un simple contrôle de défaillance à moins que l’ingénierie ne l’approuve | Dessin |
| Perpendiculité | Influence l’assise ou l’alignement des faces d’extrémité et des épaules | Indicator, surface plate setup, CMM | Nécessite une référence de référence valide | Dessin |
| Rugosité de surface | Can influence friction, Ajusté, Sortie, and galling | Testeur de rugosité de surface | Paramètre, cutoff, Direction, and location must be specified | Dessin ou spécification de surface |
| Dureté | Cela peut confirmer une nécessité de traitement thermique | Test de dureté approuvé ou documentation du fournisseur | Test scale, Emplacement, Condition de la surface, and indentation effect matter | Dessin ou spécification du matériau |
Geometric terms should be interpreted according to the drawing standard in use. ISO 1101 defines geometrical tolerancing concepts in the ISO system, tandis que ASME Y14.5 is widely used for US-oriented GD&T drawings.
A drawing that specifies runout should not be rewritten as concentricity during inspection. These controls describe different requirements and may require different measurement strategies.
SunshinePro’s tungsten-carbide punch page lists micrometer or caliper checks, projector measurement, and roughness testing for that product category. Those published methods show the types of inspection that may be relevant, but they do not prove that every punch or every order receives the same checks.
Choisissez l’instrument selon la tolérance et la caractéristique
Instrument choice should be based on the feature, Tolérance, Accès, and required measurement confidence.
| Instrument | Meilleure utilisation | Principale limitation |
| Micromètre | Diamètres et épaisseurs externes accessibles | Contact geometry may not suit small, effilé, delicate, or irregular features |
| Étrier | Identification, broad dimensions, and screening | La résolution et l’influence de l’opérateur peuvent être inadaptées aux tolérances serrées |
| Jauge de hauteur et plaque de surface | Axial dimensions, shoulder positions, and comparative height checks | Nécessite un placement contrôlé des sièges et une configuration de datum |
| Indicateur à cadran avec bloc en V ou centres | Runout, rotational variation, and some straightness checks | Les résultats dépendent fortement de la position de support et de la simulation de données |
| Comparateur optique ou système de vision | Profiles, Angles, Rayons, tip shapes, and edge form | Requires alignment, magnification control, and correct profile interpretation |
| CMM | Géométrie complexe et relations basées sur les données | Probe access, Fixation, strategy, and uncertainty must be controlled |
| Jauge go/no-go | Vérification fonctionnelle rapide d’une limite de taille | Donne les informations sur les réussites/échecs mais pas la déviation réelle ou la tendance d’usure |
| Testeur de rugosité | Vérification numérique de la texture de surface | Requires the correct parameter, Direction, cutoff, and measurement location |
Les jauges de limite lises sont couvertes par ISO 1938-1. A go/no-go gauge can be efficient for repeated checks, but variable measurement is still useful when the actual size or rate of wear matters.
Surface-texture requirements should be read from the drawing rather than inferred from appearance. ISO 21920-1 covers the indication of profile surface texture in technical product documentation.
Décider si le résultat est acceptable
A measured value is not meaningful until it is compared with an approved requirement.
Possible acceptance sources include:
- the current approved drawing;
- the purchase specification;
- the control plan;
- an approved customer deviation;
- an approved sample with defined measurement criteria;
- a documented service limit;
- a validated internal wear limit.
Nominal size alone does not determine acceptance. A drawing dimension of 10 mm, par exemple, cannot be judged without its tolerance and any related geometric or surface requirements.
Use a controlled decision process:
| Condition de résultat | Réponse requise |
| Clairement dans les exigences | Enregistrez le résultat et acceptez ou retournez la perforatrice en service |
| Proche d’une limite ou incohérent | Verify cleanliness, Température, instrument, method, Fixation, datum setup, et la répétabilité |
| En dehors de l’exigence | Mettez en quarantaine le punch et lancez le processus de non-conformité approuvé |
| La spécification manque ou est conflictuelle | Arrêtez le punch jusqu’à ce qu’une clarification écrite soit reçue |
| Défaut répété après remplacement ou rectification | Étudier le système de puces plus large et les conditions du procédé |
Measurement uncertainty becomes important near a specification limit. ISO 14253-1 provides decision rules for proving conformity or nonconformity while accounting for measurement uncertainty.
In practical terms, a borderline reading should not be accepted or rejected casually. Confirm that the instrument and method are capable of resolving the requirement, then apply the organization’s documented decision rule.
L’échantillonnage ou l’inspection à 100 % dépend des risques et des exigences contractuelles
The inspection quantity should be determined by:
- customer or contract requirements;
- characteristic criticality;
- lot size;
- supplier performance history;
- process capability;
- failure consequence;
- previous nonconformities;
- whether the result is needed for wear trending;
- the control plan.
A statement such as “100% inspected” should identify which characteristics were checked. It may mean every punch received an identification and visual check, while only selected pieces received complete dimensional inspection.
Go/no-go gauging may support rapid inspection of every piece, but it does not provide the variable data needed to evaluate size distribution or wear trends.
Utilisez une inspection de routine pour suivre l’usure avant la défaillance
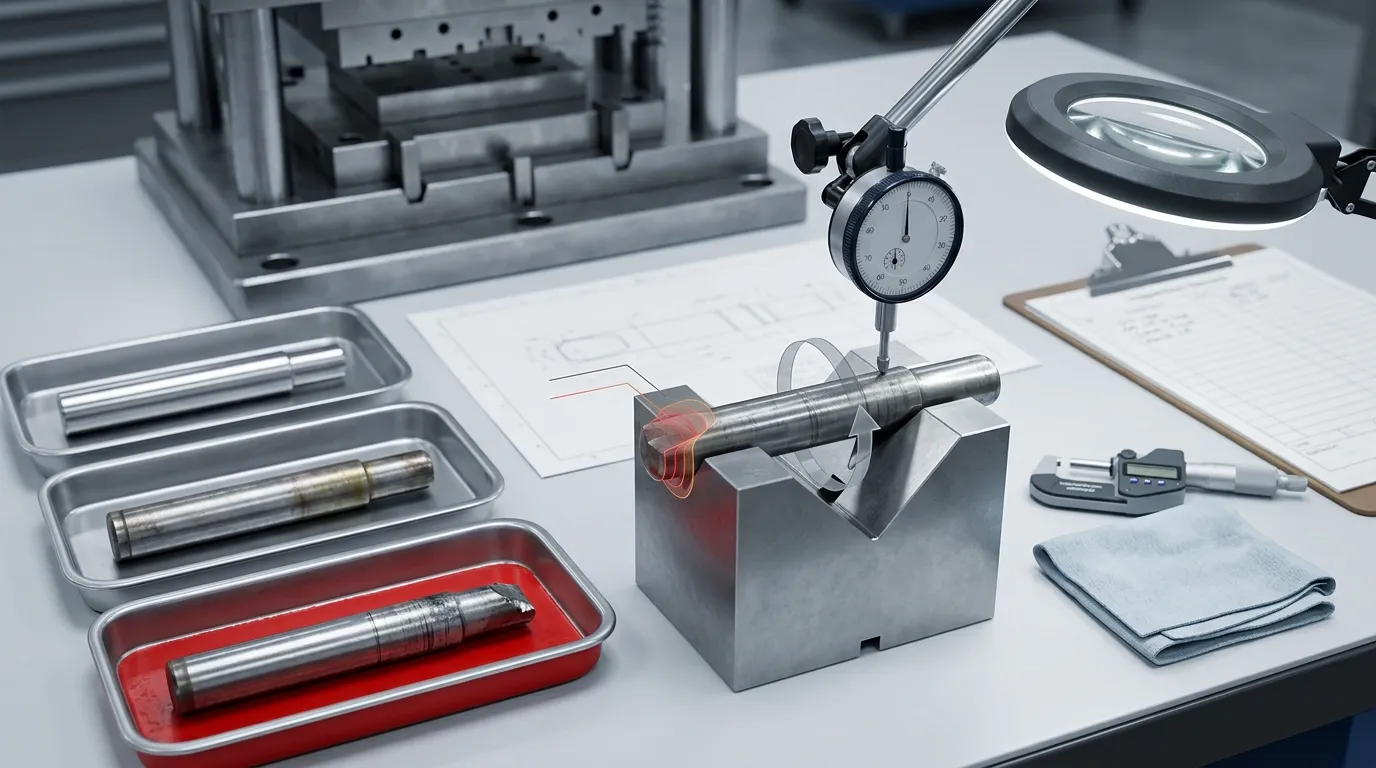
Routine QC should be based on risk and production history rather than one fixed interval for every punch.
Establish a baseline when the punch is first accepted, approved after setup, or returned from regrinding. Record dimensions and visible condition for the features most likely to change.
Trigger inspection when any of the following occurs:
- a planned production or maintenance interval is reached;
- the punch completes a high-risk or high-volume run;
- burr height or edge quality changes;
- stamped dimensions begin to drift;
- scratching or pickup appears on the part;
- stripping force increases;
- press load or operating sound changes;
- slug pulling or jamming occurs;
- a misfeed, collision, or material double-feed occurs;
- a nearby punch chips or breaks;
- the tool is removed for maintenance;
- Lubrification, stock material, or process settings change;
- the punch returns from regrinding.
Compare current values with the baseline and approved service limits. Trend data can reveal gradual wear before a dimension crosses a rejection limit.
Production symptoms should be treated as inspection triggers, Pas des diagnostics automatiques. Burrs may result from a worn punch, but they can also reflect die wear, Dégagement, Alignement, work-material variation, or stripper problems. Le Guide des matrices de poinçon provides broader context on die materials, Tolérances, Dégagement, and system-level tooling considerations.
Vérifiez à nouveau le punch après avoir remêlé ou un événement anormal
A sharp edge does not by itself prove that a reground punch is ready for service.
After regrinding, Vérifié:
- cutting-edge form;
- burr-free condition;
- Longueur totale;
- working length or projection;
- tip diameter or profile;
- surface damage or overheating;
- remaining regrind allowance, where documented;
- identification and regrind history.
After a collision, misfeed, jam, or nearby breakage, also check:
- fissures;
- permanent bending;
- head or shoulder deformation;
- runout;
- Surfaces de sièges;
- guide and retainer contact;
- the mating die opening and surrounding components.
Do not return a punch to service solely because no visible crack is present. A collision can change alignment or runout without producing an obvious surface defect.
Enregistrer le résultat et attribuer une disposition contrôlée
Inspection records should identify the punch, the requirement, the method, the result, and the final decision.
Au minimum, record:
- Numéro de pièce;
- Numéro de dessin et révision;
- supplier;
- purchase order;
- lot or serial number;
- material and coating designation;
- inspection stage;
- characteristic inspected;
- specification and tolerance;
- measured result;
- instrument identification;
- inspector;
- inspection date;
- disposition;
- Notes, photographs, or defect location where useful.
Use a controlled disposition rather than an informal “looks okay” decision.
| Découverte | Possible disposition |
| Toutes les caractéristiques requises sont conformes | Accepter ou revenir au service |
| Le résultat est incohérent ou proche d’une limite | Clean, stabilize, remeasure, or verify with a more capable method |
| La documentation manque | Maintenez ou mettez en quarantaine jusqu’à ce que des preuves soient fournies |
| Usure des bords réparables dans une limite approuvée | Envoyez demander un meulage approuvé par l’ingénierie |
| Craquement, Écaillage sévère, permanent bending, or unsafe head damage | Remplacer ou rejeter |
| La dimension est hors exigence | Quarantaine et processus en tant que non-conformes |
| Les mêmes dégâts se répètent à plusieurs reprises | Investigate clearance, Alignement, Orientation, Rétention, Lubrification, et conditions de procédé |
Nonconforming punches should be clearly identified and physically segregated so they cannot return to production accidentally.
SunshinePro states that its quality approach includes raw-material inspection, Surveillance en cours de processus, Essais finaux, measuring equipment, and inspection reports. Buyers should still define the required inspection characteristics and documentation for each order rather than assume that one standard report fits every punch.
Que demander à un fournisseur de goupilles perforatrices
A buyer should define inspection evidence before the order is released, especially for custom or critical punches.
Request the items that are relevant to the application:
- Dessin et révision approuvés;
- part, lot, and serial identification requirements;
- drawing-specific inspection report;
- material certificate or certificate of conformity;
- heat-treatment or hardness evidence where specified;
- coating documentation where specified;
- Déviations approuvées;
- packing and corrosion-protection requirements;
- identification of characteristics receiving 100% inspection;
- identification of characteristics inspected by sampling;
- measurement method for tight or complex tolerances;
- traceability between the punch, certificate, and inspection report.
Broad catalog statements are not a substitute for characteristic-level evidence. A supplier may state a general tolerance capability, but the buyer still needs confirmation that the required feature, Matériel, Géométrie, and measurement method are suitable for the specific drawing.
SunshinePro lists tool steel, Acier à grande vitesse, carbure, Usinage CNC, Rectification de précision, EDM, Traitement thermique sous vide, and drawing-based customization on its punch-related pages. These published options can support an RFQ discussion, but the exact material, Processus, Tolérance, Revêtement, and inspection documentation should be confirmed for the individual part.
Résumé de la liste de contrôle de l’inspection des goupilles de perforation
Use this condensed sequence for incoming, routine, post-regrind, and post-event inspections:
- Identify the inspection stage.
- Confirm the part number, lot or serial number, Dessin, and revision.
- Review the purchase order, control plan, and document requirements.
- Inspect packaging and record transport damage.
- Clean the punch without damaging its edge or coating.
- Verify instrument condition, Portée, Résolution, and calibration status.
- Inspect the cutting edge, Indice, Carrosserie, Tête, Épaule, Rayons, Revêtement, and identification.
- Measure the dimensions and geometric characteristics required by the drawing.
- Use an instrument suitable for the feature and tolerance.
- Compare results with the approved acceptance source.
- Verify borderline results and account for measurement uncertainty.
- Record the specification, result, instrument, inspector, et date.
- Accept, hold, quarantine, regrind, remplacer, or reject through a controlled disposition.
- Investigate the wider die system when the same damage repeatedly returns.
For a custom or replacement punch, submit the approved drawing together with the required material, Revêtement, Inspection, and documentation needs. SunshinePro La Goupille de Pointe page provides its published product context, et le Page de contact can be used to request drawing review or clarify inspection-report requirements.
Partager:



Écrit par Sunshine
Au soleil, Nous sommes un fabricant et fournisseur professionnel de composants de moule de précision, proposant une large gamme de produits pour les applications de stampage et de moulage par injection. Notre objectif principal est le poinçage des coins, Goupilles et manchons d’éjection, et poteaux guides et bagues. Avec un usinage CNC avancé, Contrôle qualité strict, et de fortes capacités de production, Nous garantissons une fiabilité, Pièces de haute précision, ainsi que des composants standards en stock pour un approvisionnement mondial rapide et efficace.
ACTUALITÉS
OBTENIR UN SERVICE
Avec des pièces de qualité adaptées à tous les budgets et un personnel accueillant formé pour rendre votre visite informative et sans tracas.
