



Inspection de la longueur de travail de la perforatrice de tablettes pour des comprimés cohérents
Tablet punch working length is the distance from the punch head flat to the lowest consistently measurable point in the punch cup. A valid inspection measures that distance directly, records every punch individually, and evaluates upper and lower punches as separate sets.
Working-length inspection can help control punch position and reduce one source of tablet thickness, Dureté, Remplissage, and weight variation. It does not guarantee consistent tablets by itself. Comportement de formulation, Performance des alimentateurs, Réglages de compression, État de presse, and other tooling dimensions also affect the finished product.
Pour des informations plus larges sur les poinçons, Ceci, and compatible tooling systems, voir Types d’outils de presse à tablette. This guide focuses only on measuring and interpreting punch working length.
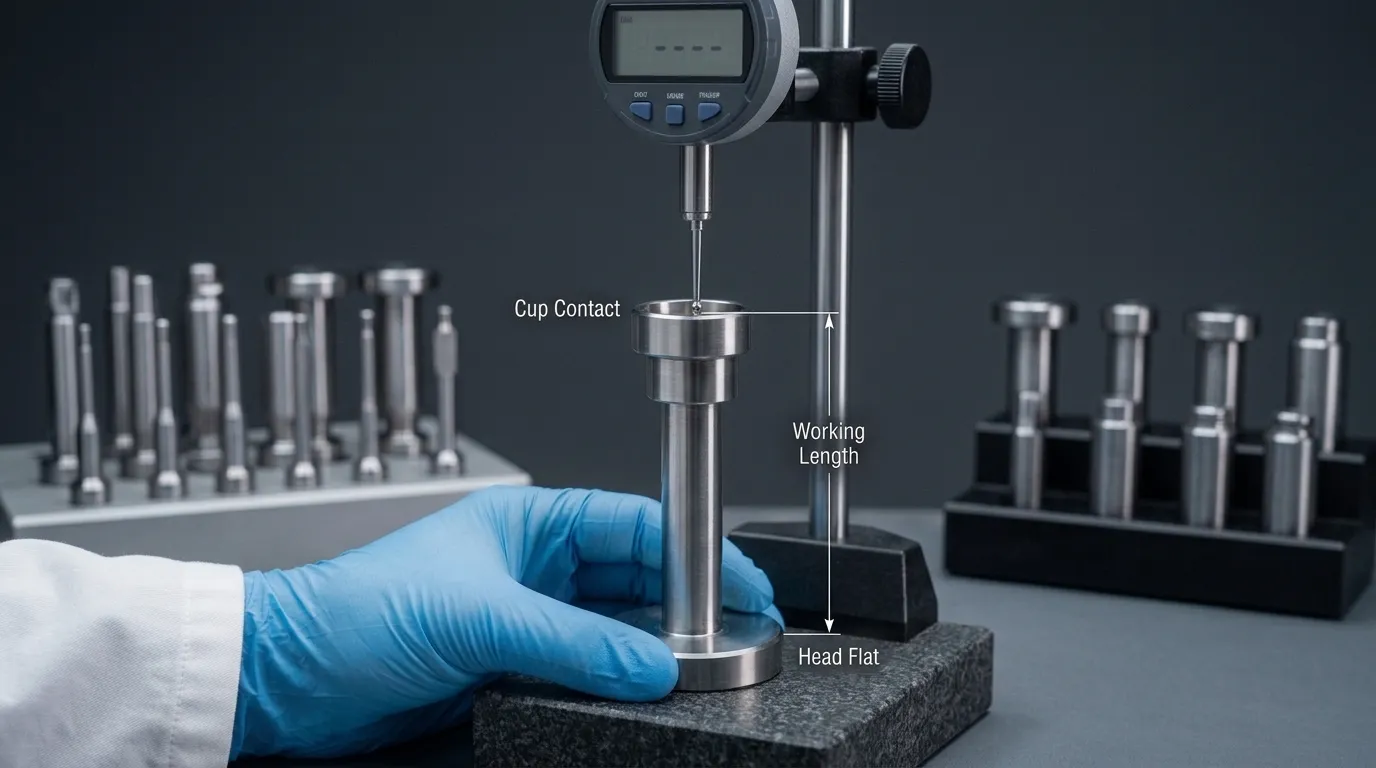
Quelle mesure la longueur de travail du poinçon—et pourquoi c’est important
A tablet punch has several dimensions, but working length is defined by two specific locations:
- The flat surface on the punch head.
- The lowest repeatable measurement point inside the punch cup.
The word “repeatable” matters. On a plain concave cup, the lowest point may be easy to contact. On an embossed, bisected, or deeply concave punch face, the measuring probe must reach the same defined location on every punch.
Working-length variation changes where individual punches operate relative to the compression rollers and die table. Selon Discussion technique de Natoli sur la longueur du punch et la profondeur du gobelet, differences within an upper-punch set can contribute to inconsistent compression conditions and variations in tablet thickness or hardness.
Lower-punch working length also affects the punch position inside the die during filling. A shorter or longer lower punch may alter the available fill volume. That can contribute to tablet-weight variation, although powder flow, feeder adjustment, and press settings remain important factors.
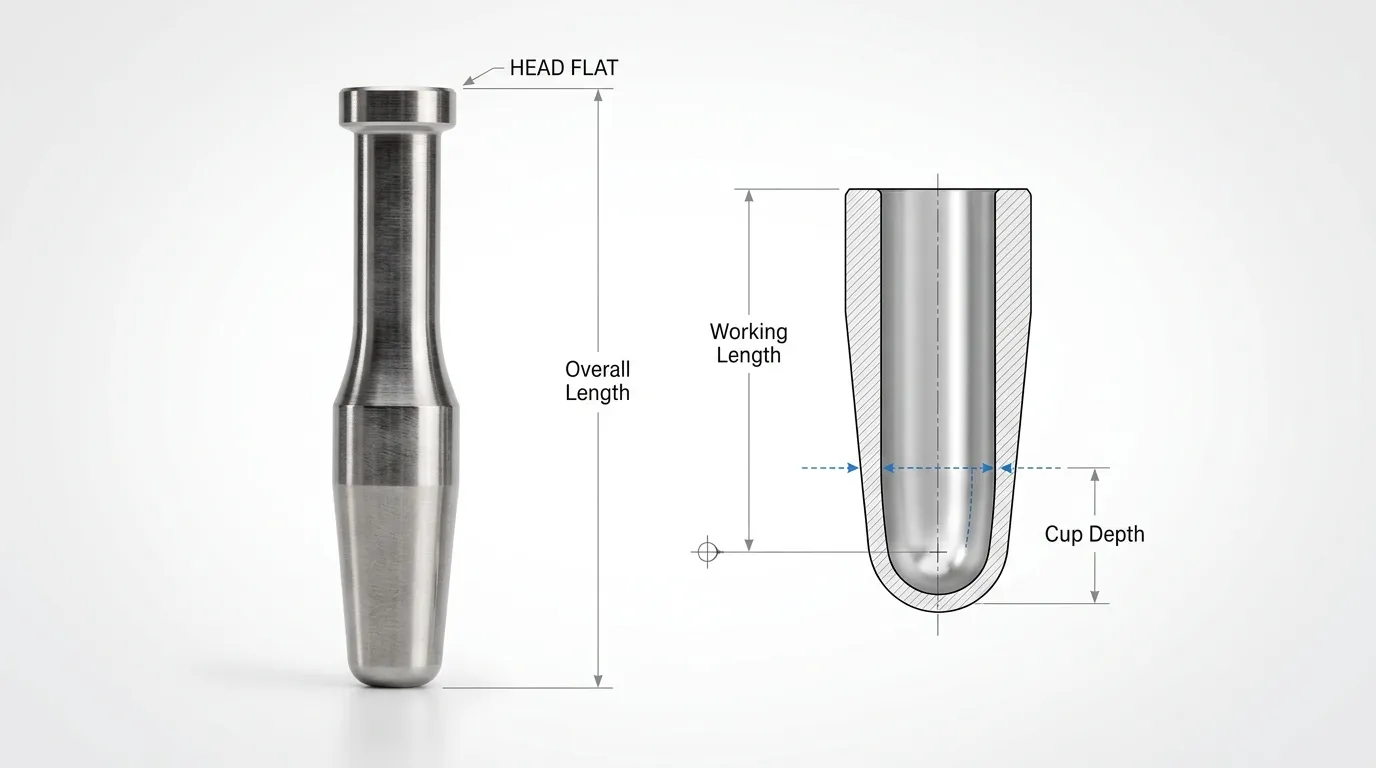
Longueur de travail vs longueur totale et profondeur de la coupe
These three measurements are related but not interchangeable.
| Dimension | Points de mesure | Main relevance |
|---|---|---|
| Longueur de travail | La tête à plat jusqu’au point le plus bas et constamment mesurable dans la coupe | Position effective du poinçon pendant le remplissage et la compression |
| Longueur totale | Surface de la tête jusqu’à l’extrémité physique la plus éloignée de la pointe du poinçon | Taille générale du punch et condition dimensionnelle |
| Cup depth | Face de pointe ou référence de terrain au point le plus profond de la coupe | Tablet shape, Volume, and cup geometry |
Working length should normally be measured directly. Calculating it by subtracting cup depth from another dimension can combine the errors of two separate measurements. Direct measurement avoids that compounded error when the cup geometry allows reliable probe access.
Établir la spécification régissant avant de mesurer
Do not begin by choosing a tolerance from an article, catalogue, or general industry reference. First identify the document that controls the actual punch set.
The inspection basis should normally follow this order:
- Approved tooling drawing and revision.
- Contractual or purchase specification.
- Approved supplier documentation.
- Internal inspection procedure.
- General industry guidance, used only when it does not conflict with controlled requirements.
Determine whether the inspection must evaluate:
- Each punch against a nominal working length.
- Variation between punches in the same set.
- Both absolute conformance and within-set consistency.
These are separate checks. A group of punches may be closely matched to one another but still fall outside the approved nominal dimension. Inversement, every punch may fall within its individual tolerance while the difference between the shortest and longest punch is too large for the approved matching requirement.
ISO 18084:2011 provides an international framework covering tablet punch-and-die dimensions, Tolérances, Caractéristiques, et interchangeabilité. Its existence does not mean every tooling set has the same working-length acceptance limit, and compliance should not be assumed unless it is stated in the applicable documentation.
Préparez le jeu de poinçons et le système de mesure
A small measurement difference is meaningful only when the measuring system can detect it consistently. Preparation should address the punches, the fixture, the instrument, and the inspection record.
Before taking readings:
- Separate upper punches from lower punches.
- Confirm the identity or set number of every punch.
- Clean the head flat and the cup contact area.
- Check for residue, meules, Dégâts, or raised material.
- Confirm that each punch can sit in the fixture without rocking.
- Select a probe that can reach the defined cup location.
- Check the indicator’s calibration status.
- Perform any required pre-use reference or zero verification.
- Confirm that the approved drawing and inspection procedure are available.
The indicator should be mounted on a rigid stand or comparable stable fixture. Movement in the base, post, probe, or punch support can appear as dimensional variation even when the punches are identical.
Calibration and verification should follow the site’s documented quality system. Le Directives de validation de l’Organisation mondiale de la santé calls for inspection instruments to be calibrated and verified under documented programmes, with defined limits, intervals, Responsabilités, Traçabilité, Records, and actions.
Résolution, Précision, and Repeatability Are Not the Same
A digital display with many decimal places is not automatically suitable for working-length inspection.
| Caractéristiques | Ce qu’il te dit |
| Résolution | Le plus petit incrément affiché par l’instrument |
| Précision | À quel point la lecture représente la valeur de référence |
| Répétabilité | À quel point la même configuration produit le même résultat de façon constante |
| Incertitude de mesure | Le doute lié au résultat rapporté |
An instrument may display very small increments while producing unstable or biased readings. The complete system—including the probe, Calendrier, seating method, Technique opératrice, and environment—must be capable relative to the applicable tolerance.
Borderline results require particular care. When the possible measurement uncertainty is large compared with the remaining distance to the acceptance limit, the reading should not be treated as unquestionable evidence.
Comment mesurer la longueur de travail d’une perforatrice de tablette
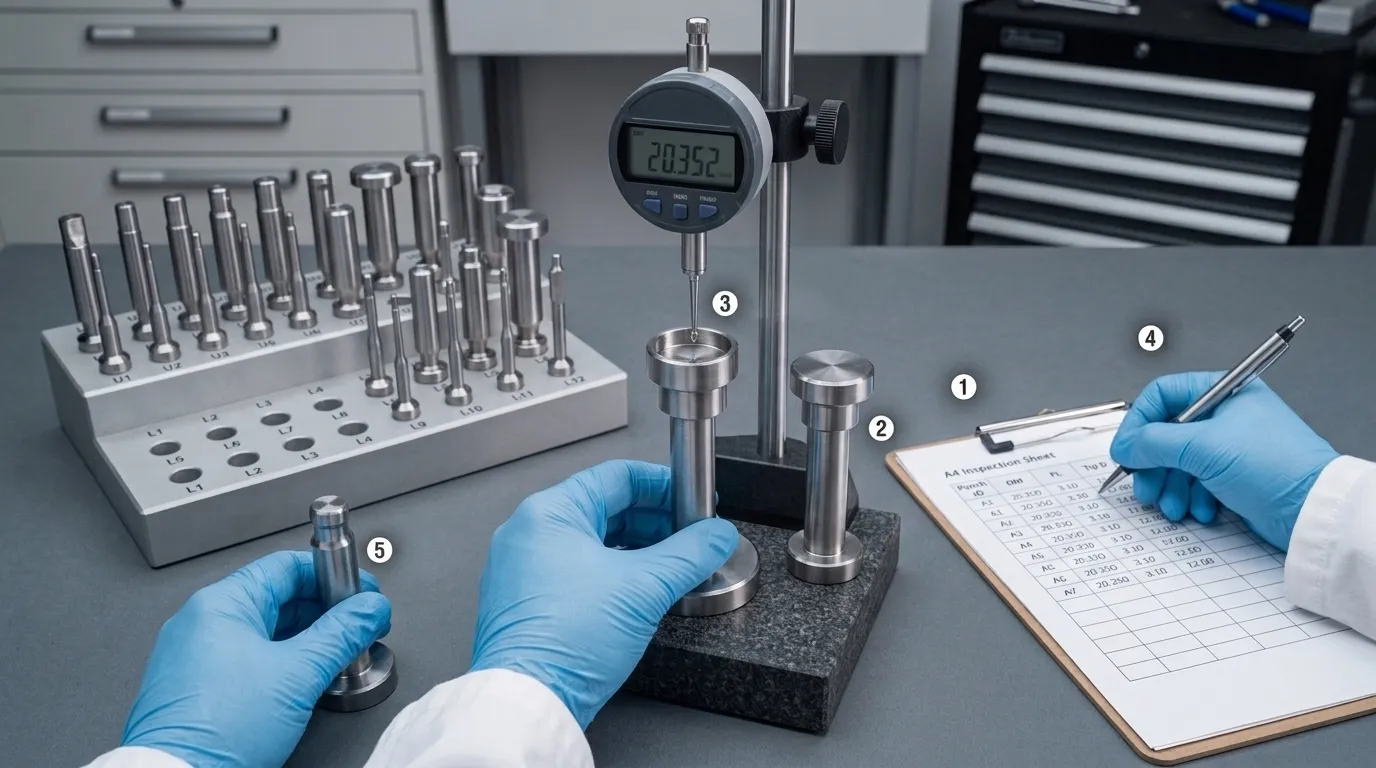
Use the approved site or supplier method where one exists. A typical direct-contact inspection follows this sequence:
- Confirm the reference condition.
Verify the indicator’s zero or reference position using the approved method. - Select the correct punch group.
Measure all upper punches as one dataset. Measure lower punches separately. - Identify the punch.
Record its unique number, set position, or other traceable identifier before taking the reading. - Seat the punch consistently.
Position the head flat against the approved support or datum. The punch must not rock, Inclinaison, or sit on residue. - Position the probe.
Bring the contact probe to the defined lowest measurable point in the cup. Use the same location and orientation for every comparable punch. - Apply the approved contact method.
Avoid excessive force. Contact pressure should be consistent and should not damage the punch surface. - Allow the reading to stabilize.
Record the actual displayed result without unnecessary rounding. - Repeat when required.
Remove and reseat the punch if the procedure calls for repeated readings. Repeated measurements help reveal seating or probe-position errors. - Continue through the complete set.
Do not stop after measuring a few apparently similar punches. A single outlier may appear anywhere in the set. - Record abnormalities immediately.
Note unstable readings, difficult probe access, visible wear, damaged surfaces, or any deviation from the approved method.
Do not compare a lower punch with the upper-punch dataset. Their dimensions and functional positions may differ even when they belong to the same tooling set.
Record Each Punch by Identity, Not Just Sequence
A useful inspection record should connect every result to the physical punch. Au minimum, Dossier:
- Punch identifier.
- Upper or lower designation.
- Tooling set or product reference.
- Numéro de dessin et révision.
- Instrument identification.
- Calibration or verification status.
- Individual reading.
- Repeated readings, Lorsque nécessaire.
- Final reported result.
- Acceptance criterion.
- Inspector and date.
- Final status or disposition.
Le Directives GMP de la Commission européenne pour le contrôle qualité supports maintaining procedures and records for specifications, Essais, calculations, equipment calibration, approval or rejection, and instrument identification.
Calculer et interpréter les résultats de l’inspection
After measuring the complete upper or lower punch set, identify:
- The minimum working-length reading.
- The maximum working-length reading.
- The difference between them.
Use this calculation:
Plage de longueur de travail = lecture maximale − lecture minimale
Par exemple, consider an illustrative upper-punch dataset:
| Punch | Longueur de travail |
| U01 | 133,602 mm |
| U02 | 133,599 mm |
| U03 | 133,604 mm |
| U04 | 133,601 mm |
The minimum is 133.599 mm and the maximum is 133.604 mm.
Range = 133.604 − 133.599 = 0.005 mm
This example demonstrates the calculation only. It does not establish an acceptable limit.
Interpret the data in two stages:
- Compare every punch with the approved nominal dimension and tolerance.
- Compare the set’s maximum-to-minimum range with the approved matching or variation requirement.
A punch set should not be accepted solely because the readings are close together. All punches could be similarly short or similarly long. The nominal dimension and within-set range both need review when the specification requires both.
Why a Common 0.002-Inch Figure Is Not a Universal Limit
Some specialist tooling sources cite a maximum working-length variation of 0.002 inch within a punch set. This figure may be useful as industry context, but it should not automatically be applied to every press, Norme d’outillage, Produit, or inspection programme.
The controlling limit must come from the approved drawing, supplier agreement, or internal procedure. The public summary of ISO 18084 does not establish 0.002 inch as a universal working-length acceptance criterion.
Handle Embossed, Bisected, Deep-Cup, and Multi-Tip Punches
Complex punch geometry can make a normal contact measurement unreliable.
| Fonction de poinçon | Risque de mesure | Réponse appropriée |
| Embossage | La sonde entre en contact avec un caractère en relief au lieu du point de coupe défini | Utilisez un emplacement spécifié qui évite la caractéristique embossée |
| Droite de bisecte | La sonde atterrit sur le score ou de côtés différents entre les coups de poing | Définir une orientation et une position de contact cohérentes |
| Coupe profonde concave | La sonde ne peut pas atteindre le point le plus bas sans interférence | Utiliser une sonde adaptée ou une méthode alternative approuvée |
| Coupe irrégulière | Le point le plus bas est difficile à reproduire | Établissez un équipement documenté et une orientation |
| Poinçon multi-types | Une lecture globale peut masquer les différences entre les conseils | Évaluez les conseils individuels lorsque la spécification l’exige |
Never move the probe to whichever location is easiest on each punch. Changing the contact location can create apparent variation that comes from geometry rather than actual working-length differences.
Where the lowest point cannot be contacted consistently, a different probe, custom fixture, profile-measurement method, or non-contact inspection system may be more appropriate. Discussion de Pharmaceutical Technology sur la technologie d’inspection des outillages describes the use of data-capture and non-contact systems for more complex or automated inspection tasks.
Confirmez si une lecture anormale est une véritable anomalie de coup de poing
One abnormal reading should trigger verification, not an immediate decision to reject or alter the punch.
Utilisez cette séquence:
- Recheck the punch identifier.
- Clean the head flat, support surface, and cup contact area.
- Inspect for burrs, Résidu, Dégâts, ou déformation.
- Confirm that the punch is seated correctly.
- Verify the probe location and orientation.
- Recheck the instrument reference.
- Remove, reseat, and measure the punch again.
- Compare repeated readings.
- Escalate the result if the abnormal value remains stable.
If the repeated values move substantially, the measurement setup may be unstable. If repeated readings remain close to one another but differ from the rest of the set, the punch is more likely to have a real dimensional difference.
Causes courantes d’un changement réel de longueur de travail
Once measurement error has been ruled out, possible causes include:
- Wear on the punch head flat.
- Uneven or excessive polishing.
- Physical damage or deformation.
- A replacement punch that was not matched to the existing set.
- Upper and lower punches mixed incorrectly.
- Manufacturing or refurbishment variation.
- An incorrect punch from another tooling set.
Ne pas polir, grind, or otherwise alter a suspected punch before the dimensional condition has been documented and the proper disposition has been approved.
Decide Whether to Accept, Investigate, Quarantaine, Refurbish, ou Remplacer
The confirmed measurement and the governing specification should determine the next action.
| Découverte | Réponse contrôlée typique |
| Chaque poinçon répond aux exigences nominales et de variation en ensemble | Accepter et documenter |
| Une lecture est instable ou non reproductible | Examinez la configuration et remesurez |
| Un résultat est proche d’une limite d’acceptation | Faites l’examen de l’incertitude et suivez le processus d’escalade approuvé |
| Un coup de poing diffère systématiquement de l’ensemble | Quarantine and evaluate matching, Rénovation, ou remplacement |
| Plusieurs coups montrent un raccourcissement progressif | Investigate wear, État de presse, Manipulation, or maintenance practice |
| Une surface de référence est endommagée | Mettre en quarantaine et évaluer l’adéquation de la réparation ou du remplacement |
| L’identité de l’outil ne peut pas être confirmée | Maintenez l’outillage jusqu’à ce que la traçabilité soit rétablie |
| L’ensemble ne remplit pas l’exigence approuvée | Follow the site procedure for rejection, Rénovation, ou remplacement |
Refurbishment is not automatically suitable for every failed punch. Any corrective work can alter critical dimensions and must be followed by appropriate inspection.
Replacement punches should also be evaluated against the existing set rather than treated as acceptable only because they match a nominal catalogue value.
Documentez l’inspection et la modification de la voie au fil du temps
A one-time result shows the current condition. A series of traceable inspections can reveal how the tooling changes during service.
The inspection record should retain:
- Individual punch readings.
- Upper- and lower-set ranges.
- Drawing and revision information.
- Instrument and verification details.
- Any remeasurement activity.
- Visible wear or damage.
- Acceptance decision.
- Quarantaine, Rénovation, or replacement action.
Where previous records exist, compare the same punch over time. A gradual reduction in working length may indicate progressive head-flat wear even before the punch exceeds a formal limit.
Trend review should follow approved site rules. Do not create informal warning limits without technical justification, risk assessment, and authorization.
Broader cleaning, Stockage, Manipulation, Lubrification, and inspection-frequency controls belong in a complete Liste de contrôle pour la maintenance des outils de tablette.
Que demander dans un rapport de correspondance de fournisseurs
When ordering a replacement punch or a matched tooling set, useful supplier documentation may include:
- Individual punch identification.
- Upper or lower designation.
- Numéro de dessin et révision.
- Actual working-length readings.
- Measurement method.
- Stated acceptance criterion.
- Instrument or calibration reference, Lorsque cela est disponible.
- Matching or grouping information.
- Final inspection status.
Do not assume every supplier provides the same report. Confirm the documentation requirements before placing the order.
Discutez des exigences de remplacement ou de perforation personnalisée avec le dessin disponible
When an inspection confirms a mismatch, damaged punch, or replacement need, prepare the technical information before contacting a supplier:
- Dessin et révision approuvés.
- Tooling type.
- Upper or lower punch designation.
- Existing punch identifiers.
- Individual working-length results.
- Maximum-to-minimum range.
- Description of visible wear or damage.
- Required material or other confirmed drawing requirements.
- Whether one replacement punch or a complete matched set is being considered.
- Documentation d’inspection requise.
SunshinePro présente Presse à tablettes perfore et matrice and states that custom tooling can be processed from drawings or samples. The product page also lists high-speed steel and customized size or material options.
For a replacement or custom-tooling enquiry, send the applicable drawing and inspection results through the Page de contact SunshinePro and ask the company to confirm feasibility, measurement documentation, and the specification that would apply to the supplied tooling.
Partager:



Écrit par Sunshine
Au soleil, Nous sommes un fabricant et fournisseur professionnel de composants de moule de précision, proposant une large gamme de produits pour les applications de stampage et de moulage par injection. Notre objectif principal est le poinçage des coins, Goupilles et manchons d’éjection, et poteaux guides et bagues. Avec un usinage CNC avancé, Contrôle qualité strict, et de fortes capacités de production, Nous garantissons une fiabilité, Pièces de haute précision, ainsi que des composants standards en stock pour un approvisionnement mondial rapide et efficace.
ACTUALITÉS
OBTENIR UN SERVICE
Avec des pièces de qualité adaptées à tous les budgets et un personnel accueillant formé pour rendre votre visite informative et sans tracas.
