



Résistance à l’usure dans les composants de moule: Matériaux, Revêtements, and Heat Treatment
Wear resistance in mold components depends on choosing the right steel, Revêtement, and heat treatment for the molding environment. Abrasive plastics, sliding contact, and high production cycles can quickly damage cores, Cavités, et systèmes d’éjection. Hardened tool steels, Nitrage, and wear-resistant coatings help reduce maintenance, improve dimensional stability, and extend mold life when matched correctly to the application.
Mold wear is one of the biggest reasons injection molds lose accuracy over time. Gates begin to flash, sliders start galling, and polished surfaces lose consistency. Many of these failures are preventable with better material selection and surface engineering. This guide explains how wear develops in mold components, which materials perform best, and how coatings and heat treatment affect long-term tooling performance.
What causes wear in mold components?
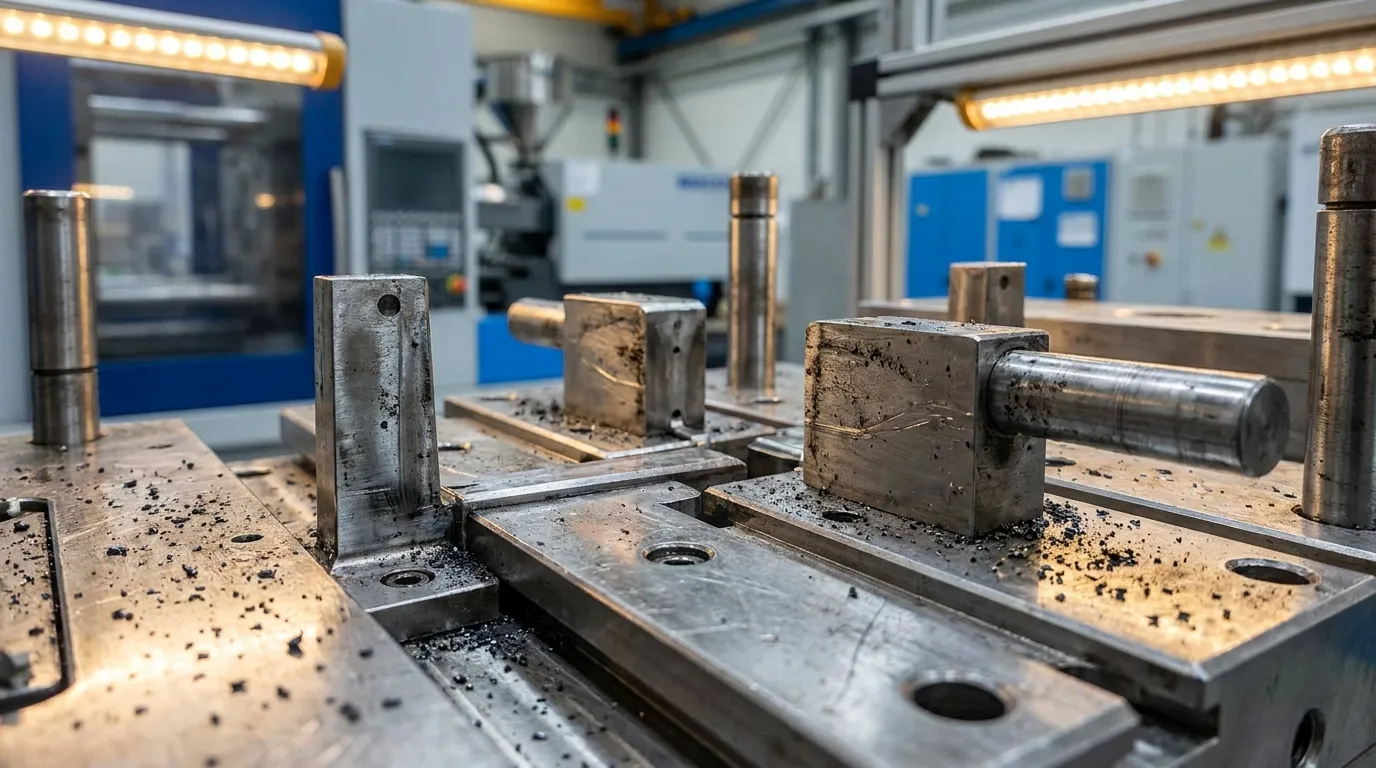
Wear resistance in mold components depends on controlling abrasion, Friction, and surface fatigue. Résines remplies de verre, Mauvaise lubrification, and repeated cycling accelerate wear on cores, Cavités, Goupilles éjecteurs, and sliding components.
Most mold wear comes from repeated friction between steel surfaces and abrasive plastic flow. Filled engineering plastics are especially damaging because glass fibers and mineral additives scrape the mold surface during every injection cycle. Over time, this removes material from gates, cores, and shutoff surfaces.
Selon une recherche résumée par ScienceDirect, wear resistance is affected by hardness, Force, Rugeose de surface, and material structure. In mold tooling, those properties work together rather than independently.
Usure abrasive vs adhésive dans les moules
Abrasive wear happens when hard particles cut into the mold surface. This is common with glass-filled nylon, flame-retardant compounds, and mineral-filled resins. Gate inserts and runner transitions usually show the first signs of damage.
Adhesive wear happens when two metal surfaces rub against each other under pressure. Slides, lifters, and ejector systems are common failure points. If lubrication is poor, the surfaces may begin galling, which creates scratches, drag marks, and dimensional drift.
| Type d’usure | Cause commune | Zones typiques de moisissure |
|---|---|---|
| Usure abrasive | Résines remplies de verre | Portes, Cavités, cores |
| Usure des adhésifs | Contact métallique coulissant | Slides, lifters, Éjecteurs |
| Fatigue de surface | Cyclage répété | Shutoffs, moving inserts |
| Usure corrosive | Additifs agressifs | Vent areas, Cavités |
Is hardness the same as wear resistance?
Hardness improves resistance to indentation, but wear resistance depends on toughness, Condition de la surface, lubrication, and coating performance. Extremely hard mold steels can still fail if brittleness increases.
Hardness and wear resistance are closely related, but they are not identical properties. A harder steel usually resists scratching and abrasive damage better than a softer steel. Toujours, extremely high hardness can reduce toughness and increase cracking risk under impact or cyclic stress.
Recherches discutées par SilcoTek explains that wear performance depends on the entire surface system. Material structure, friction conditions, Revêtements, and operating loads all affect long-term durability.
This matters in mold manufacturing because the hardest steel is not always the safest choice. A high-impact mold with moving slides may perform better with slightly lower hardness and better toughness. That tradeoff often reduces unexpected downtime and expensive repairs.
For molds that require advanced thermal processing, a detailed overview of Traitement thermique par moisissure can help clarify how hardness targets affect mold performance.
| Propriété | Ce que cela améliore | Risque potentiel |
|---|---|---|
| Forte dureté | Résistance à l’abrasion | Fragilité |
| Forte robustesse | Résistance aux fissures | Usure plus rapide |
| Revêtement de surface | Friction réduite | Défaillance du revêtement si le substrat est faible |
Which mold components experience the most wear?
Gate areas, Goupilles éjecteurs, diapositives, and core features typically wear fastest because they experience concentrated friction, Pression, and repeated resin flow. Abrasive fillers like glass fiber increase damage significantly.
Not every mold component wears at the same rate. High-contact and high-flow areas usually fail first, especially in molds running abrasive engineering plastics. Concentrated pressure and repeated motion accelerate material loss over time.
The following components typically require the highest wear resistance:
- Inserts de grille exposés à un écoulement rapide de résine
- Goupilles éjectrices avec mouvements glissants répétitifs
- Broches de noyau gérant la géométrie à paroi mince
- Glissières et poussoirs sous pression latérale
- Cavités moulant des matériaux remplis de verre
A mold producing glass-filled nylon electrical connectors may show gate wear after only 250,000 cycles if the tooling steel is untreated. In many cases, nitrided H13 steel lasts significantly longer than untreated H13 under the same production conditions.
For a broader overview of mold architecture and tooling functions, le Guide des composants du moule explains how these parts interact during injection molding cycles.
Which mold steels offer the best wear resistance?
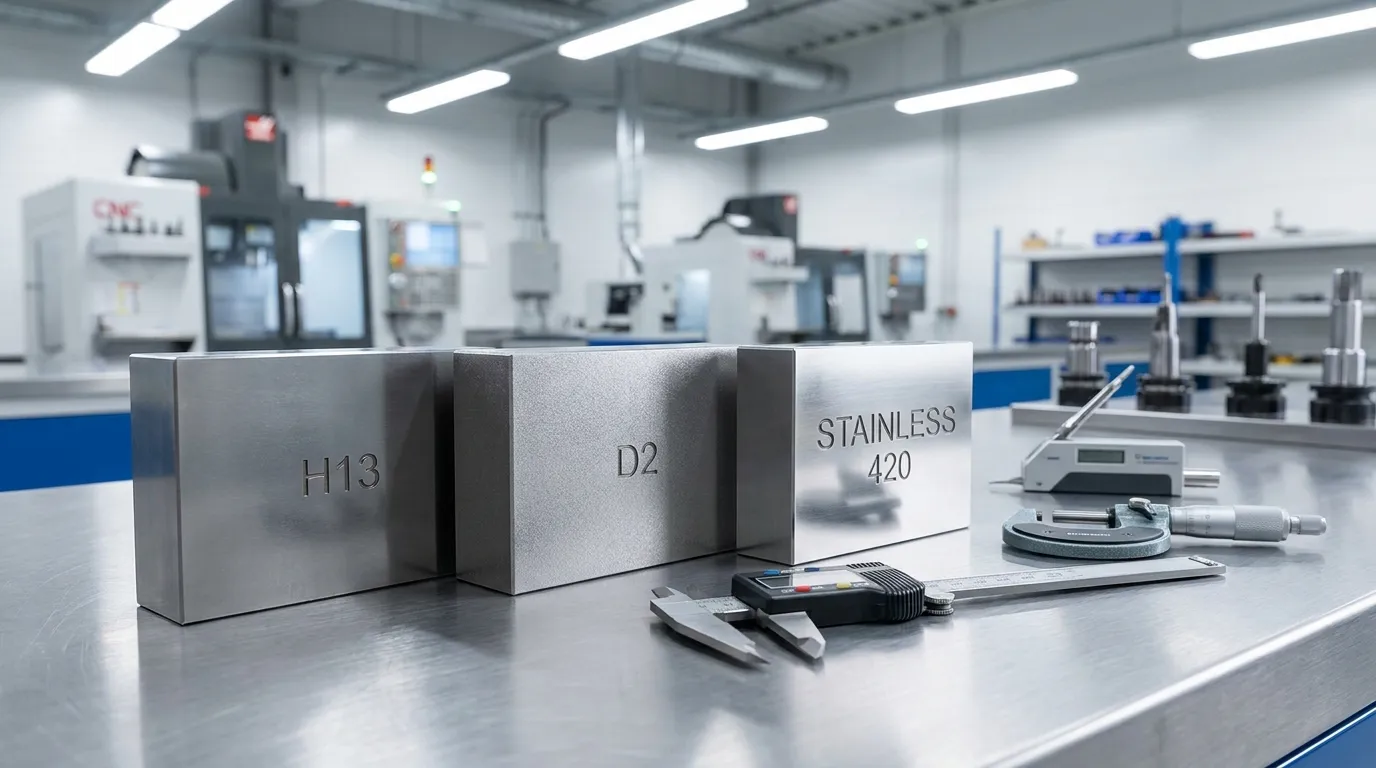
High-wear molding applications often use hardened tool steels like H13, D2, and powder metallurgy grades. The best choice depends on resin abrasiveness, Exposition à la corrosion, polish requirements, and expected cycle count.
Tool steel selection affects both mold life and maintenance cost. Different steels perform better under different molding conditions, especially when abrasive or corrosive plastics are involved.
H13 is one of the most common mold steels because it balances hardness, toughness, and machinability. D2 offers higher abrasion resistance but can become brittle in impact-heavy applications. Stainless grades like S136 improve corrosion resistance, though some stainless steels have lower wear performance than hardened tool steels.
Recherche de Stainihard notes that many austenitic stainless steels prioritize corrosion resistance over abrasion resistance. That distinction matters in molds running aggressive fillers or high-cycle production.
Choisir l’acier pour les plastiques remplis de verre
Glass-filled materials create extreme abrasive wear near gates and thin flow channels. Standard pre-hardened steels often wear too quickly in these environments. Powder metallurgy steels or nitrided H13 are more common choices for long production runs.
A cosmetic housing mold creates another tradeoff. Extremely hard tooling may improve wear life, but it can also complicate polishing and surface finishing. Dans ces cas, balanced hardness and polishability are usually safer than maximum hardness.
| Qualité de l’acier | Points forts | Limitations | Meilleure utilisation |
|---|---|---|---|
| H13 | Ténacité et stabilité thermique | Résistance modérée à l’usure | Moules de production générale |
| D2 | Forte résistance à l’abrasion | Ténacité plus faible | Résines abrasives |
| S136 | Résistance à la corrosion | Usure moindre que certains aciers à outillage | Moules médicaux et cosmétiques |
| Aciers CPM | Excellentes performances d’usure | Coût plus élevé | Moulage abrasif à grand volume |
For readers comparing broader tooling systems, le Bases du moule en plastique page explains how mold design choices affect long-term production performance.
How do coatings improve mold wear resistance?
Surface coatings improve mold wear resistance by reducing friction, surface fatigue, and abrasive damage. Coatings work best when matched with the correct substrate hardness and molding application.
Coatings protect the mold surface rather than changing the entire steel structure. They are commonly used in high-cycle molds where sliding friction or abrasive resin flow causes premature wear.
Physical vapor deposition (PVD) coatings create thin, hard surface layers that reduce friction and improve abrasion resistance. Diamond-like carbon (DLC) coatings are often used on sliding components because they reduce galling and sticking. Nitriding improves surface hardness by diffusing nitrogen into the steel surface.
Selon les directives de test d’usure publiées par TWI Global, pin-on-disc testing is commonly used to evaluate coating wear performance under friction conditions.
Lorsque les revêtements échouent prématurément
Coatings are not a substitute for poor steel selection. A premium coating applied to weak substrate material often fails faster than properly hardened tool steel without coating. Surface preparation and heat treatment quality still matter.
A high-volume automotive mold may use coated slides to reduce galling and maintenance downtime. If the base steel lacks sufficient hardness, the coating can crack or delaminate under repeated pressure.
| Type de revêtement | Principal avantage | Applications courantes |
|---|---|---|
| Revêtement PVD | Réduction de l’abrasion | Portes, cores |
| Revêtement DLC | Friction moindre | Slides, Éjecteurs |
| Nitrurage | Durcissement de surface | Outillages généraux de moule |
| Chromation | Protection contre la corrosion | Surfaces cavitaires sélectionnées |
Les moules nécessitant des finitions esthétiques combinent souvent des revêtements avec des revêtements spécialisés Options de finition de surface to maintain appearance quality and reduce polishing frequency.
Which heat treatments improve wear resistance in mold tooling?
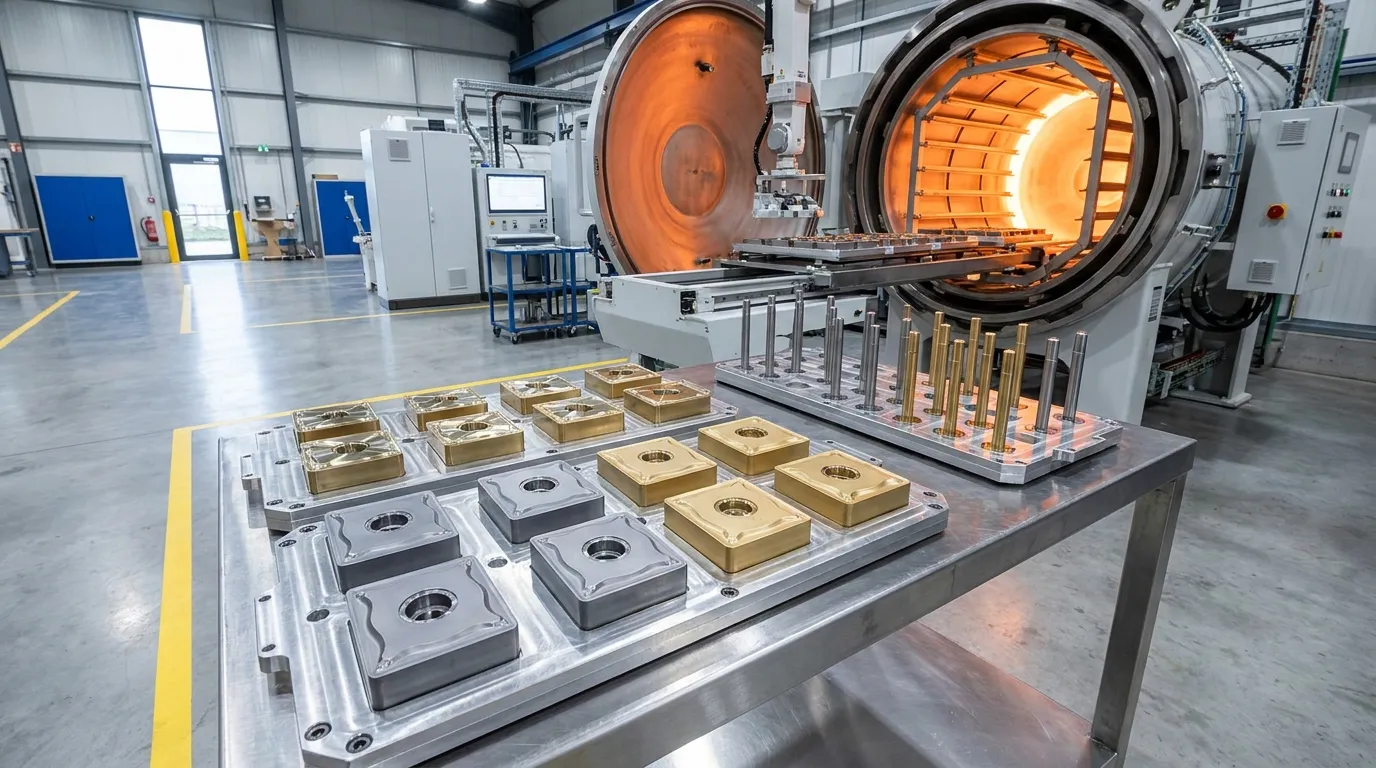
Heat treatment improves mold wear resistance by increasing surface hardness and stabilizing the steel structure. The wrong process can also increase brittleness, Distorsion, or cracking risk.
Heat treatment changes the internal structure of the steel. In mold manufacturing, this process affects hardness, toughness, Stabilité dimensionnelle, and long-term durability.
Vacuum hardening is commonly used because it limits oxidation and supports consistent hardness throughout the mold component. Tempering follows hardening and helps reduce brittleness by relieving internal stress. Case hardening and nitriding improve surface hardness without fully hardening the entire part.
Pourquoi la nitrage est-elle courante dans les moules d’injection
Nitriding creates a hard outer layer while maintaining a tougher core underneath. That balance works well for slides, Systèmes d’éjection, and components exposed to repeated friction. It also reduces distortion risk compared to some deeper hardening processes.
A mold running mineral-filled flame-retardant resin may experience rapid ejector pin wear. In many cases, nitrided ejector systems extend maintenance intervals and reduce galling problems.
| Traitement thermique | Principal avantage | Risque commun |
|---|---|---|
| Durcissement sous vide | Dureté uniforme | Distorsion si non contrôlée |
| Trempe | Soulagement du stress | Dureté réduite si excessive |
| Nitrurage | Résistance à l’usure de surface | Profondeur limitée |
| Durcissement | Extérieur dur | Complexité du procédé |
Une explication détaillée de Procédé de traitement thermique methods can help engineers match steel grades with suitable hardening strategies.
How do abrasive plastics reduce mold life?
Abrasive engineering plastics can rapidly damage mold surfaces, especially around gates and high-flow regions. Glass-filled resins often require upgraded steel grades, Revêtements, or nitrided surfaces.
Filled plastics behave differently from standard commodity resins. Glass fibers, flame retardants, and mineral additives increase friction against the mold surface during every injection cycle. High-flow regions typically show wear first.
Glass-filled nylon is one of the most common causes of premature mold wear. Gates lose dimensional accuracy, core surfaces become rougher, and flash begins appearing earlier in production runs.
| Type de résine | Risque d’usure | Recommandation typique |
|---|---|---|
| Standard PP | Low | Acier pré-trempé |
| Nylon rempli de verre | Haut | Acier trempé ou nitruré |
| Composés ignifuges | Moyen à élevé | Outillage revêtu |
| Résine remplie de minéraux | Haut | Inserts résistants à l’usure |
A low-volume prototype mold may avoid expensive coatings because production volume does not justify premium treatment costs. High-volume production molds usually benefit from stronger wear protection because maintenance downtime becomes far more expensive over time.
Processing temperatures, Pression d’injection, and resin flow speed also influence wear behavior. Following proper Directives pour les moulures can help reduce unnecessary tooling stress.
How do you choose the right wear-resistance strategy?
The best wear-resistance strategy balances tooling cost, Volume de production, Abrasivité de la résine, and maintenance downtime. Overengineering the mold can waste budget, while underengineering increases repair frequency.
There is no single material or coating that works for every mold. The correct choice depends on resin type, expected cycle count, exigences cosmétiques, and budget limitations.
High-volume automotive tooling usually justifies premium steels and coatings because downtime costs are high. Prototype molds and short production runs often use lower-cost tooling strategies instead.
Table de décision sur l’usure de la moisissure
| Scénario de production | Acier recommandé | Revêtement ou traitement | Risque de maintenance |
|---|---|---|---|
| Prototype à faible volume | Acier pré-trempé | Traitement minimal | Modéré |
| Moule de boîtier cosmétique | S136 | Nitrie légère | Faible à modéré |
| Moule en nylon rempli de verre | Acier H13 ou CPM | Nitruration ou DPV | Low |
| Moule automobile à grande vitesse | Acier D2 ou CPM | DLC ou PVD | Très bas |
| Moule en résine rempli de minéraux | Acier à outils trempé | Nitrurage | Modéré à faible |
A mold producing abrasive parts around the clock may recover coating costs quickly through reduced maintenance. En revanche,, a short-run mold may never recover that added expense.
Les lecteurs évaluant le ROI des outils peuvent comparer de manière plus large Analyse du coût des outillages factors when deciding how much wear protection makes financial sense.
What maintenance signs indicate poor wear resistance?
Poor wear resistance usually appears gradually before major tooling failure occurs. Early warning signs include flash, Dérive dimensionnelle, polishing frequency increases, and rough surface finishes.
Slides and ejector systems may begin sticking or galling. Gates can lose edge definition, especially in molds processing abrasive fillers. Surface scratches and drag marks often appear before more serious dimensional issues develop.
Liste de contrôle pour le dépannage de l’usure
| Symptôme | Probable Cause | Solution recommandée | Urgence |
|---|---|---|---|
| Éclair à l’arrêt | Usure de surface | Retravail ou insert plus dur | Haut |
| Gallage sur les glissières | Mauvaise lubrification ou défaillance du revêtement | Revêtement ou nitruration | Moyen |
| Polissage fréquent | Usure abrasive de la résine | Améliorer l’acier ou le revêtement | Moyen |
| Finition brute à cavité | Fatigue de surface | Examen du traitement de surface | Moyen |
| Broche éjectrice coincée | Usure des adhésifs | Traitement de surface plus dur | Haut |
Preventive maintenance matters as much as material selection. Even premium tooling can wear prematurely if lubrication, Refroidissement, or processing conditions are poorly controlled.
Réussir la prochaine étape
Choosing the right wear resistance strategy starts with understanding the molding environment. Abrasivité de la résine, Volume de production, Exigences de finition de surface, and maintenance expectations all affect tooling decisions.
Many mold failures come from mismatched material choices rather than poor manufacturing. Harder steel is not always better, and coatings are not magic fixes for weak substrates. The most reliable molds use balanced engineering decisions across steel selection, Traitement thermique, and surface protection.
If your mold is already showing gate wear, Irritant, or dimensional drift, reviewing the tooling material and treatment process is usually the best place to start.
Questions fréquemment posées
What is wear resistance in mold components?
Wear resistance is the ability of a mold component to resist material loss caused by friction, Abrasion, and repeated molding cycles. Better wear resistance helps molds maintain dimensional accuracy and surface quality during longer production runs.
Does higher hardness always improve wear resistance?
Non. Higher hardness can improve abrasion resistance, but excessive hardness may reduce toughness and increase cracking risk. Mold performance depends on balancing hardness, toughness, Revêtements, et conditions de fonctionnement.
Which mold steel is best for glass-filled plastics?
Hardened tool steels such as H13, D2, and some powder metallurgy grades are commonly used for abrasive glass-filled materials. The best option depends on corrosion exposure, polish requirements, et volume de production attendu.
How do coatings improve mold life?
Coatings reduce friction, surface fatigue, and abrasive wear on mold surfaces. Properly matched coatings can extend maintenance intervals and reduce premature wear in high-cycle molding applications.
What causes rapid wear in injection molds?
Résines abrasives, Mauvaise lubrification, sliding friction, and high production cycles are common causes of rapid mold wear. Glass fibers and mineral fillers are especially damaging to gates, cores, and sliding surfaces.
Is nitriding good for mold components?
Oui. Nitriding improves surface hardness and wear resistance while maintaining core toughness. It is commonly used for slides, Systèmes d’éjection, and tooling exposed to repetitive friction.
Partager:



Écrit par Sunshine
Au soleil, Nous sommes un fabricant et fournisseur professionnel de composants de moule de précision, proposant une large gamme de produits pour les applications de stampage et de moulage par injection. Notre objectif principal est le poinçage des coins, Goupilles et manchons d’éjection, et poteaux guides et bagues. Avec un usinage CNC avancé, Contrôle qualité strict, et de fortes capacités de production, Nous garantissons une fiabilité, Pièces de haute précision, ainsi que des composants standards en stock pour un approvisionnement mondial rapide et efficace.
ACTUALITÉS
OBTENIR UN SERVICE
Avec des pièces de qualité adaptées à tous les budgets et un personnel accueillant formé pour rendre votre visite informative et sans tracas.
