



Exigences de finition de surface des goupilles de poinçon pour l’usure et le détachage
Surface finish is one of the most overlooked specifications on a punch pin, yet it directly controls two separate performance outcomes: how long the pin resists wear, and how cleanly it releases the slug or formed material after each stroke. A typical punch pin surface finish requirement calls for a fine, controlled roughness value achieved through precision grinding or lapping, not simply the tightest number available. Punch pins are one of several die components covered in our Guide des composants de la puce (déduit), but the finish spec deserves its own explanation because getting it wrong causes two very different failure modes: premature wear on one side, and sticking or galling on the other.
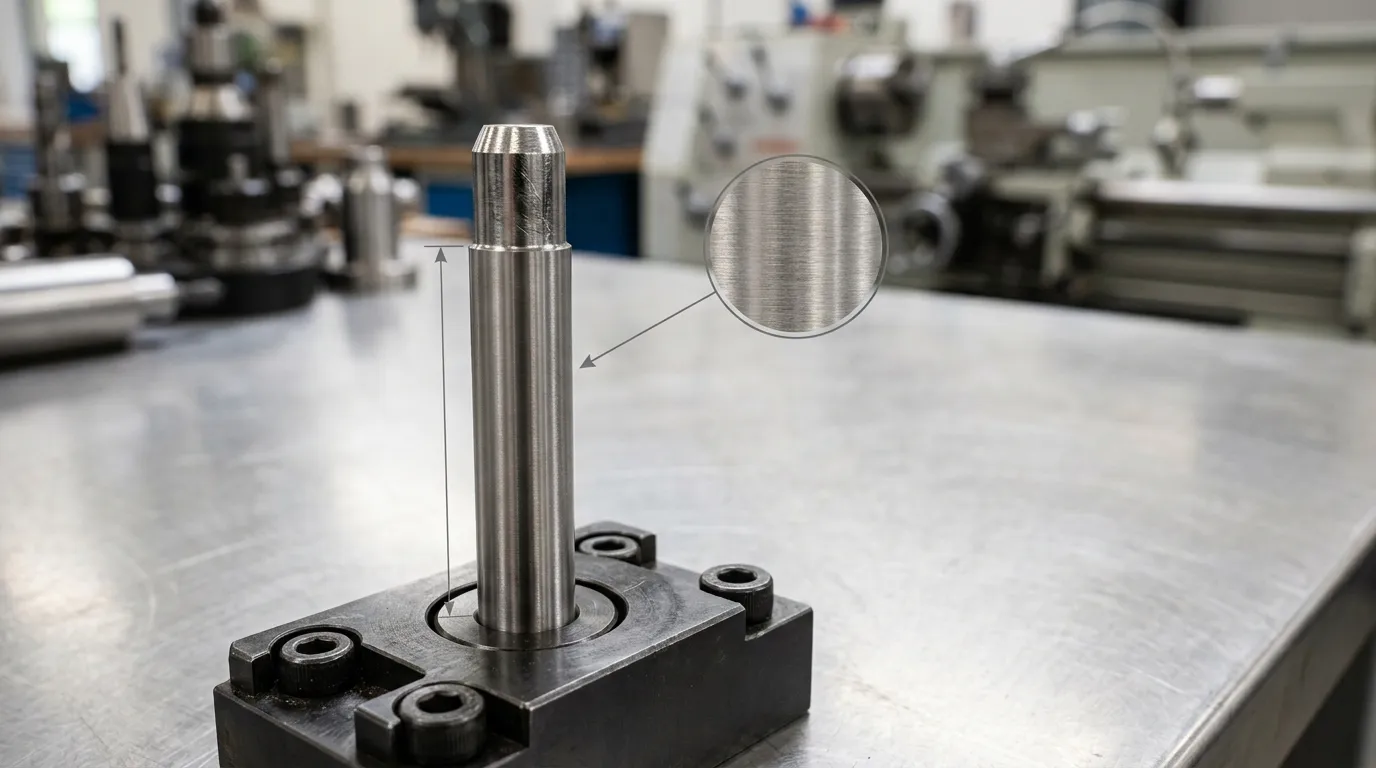
Valeurs recommandées de finition de surface pour les goupilles de perforation
Punch pin surface finish is almost always specified as a roughness average (Ra), expressed in micrometers or microinches, rather than as a visual or subjective grade. Sunshine's punches and pins are manufactured to a Ra0.4 finish with tolerances held within ±0.002 mm, giving a concrete benchmark for what a precision-ground punch pin surface looks like in practice.
Cela étant dit, "the right finish" depends on the application. A punch pin running high cycle counts against abrasive sheet stock needs tighter control than one used in low-volume, low-friction operations. For context, general machining references classify finer finishes (roughly 0.8 µm Ra and below) as suitable for sealing or precision-fit surfaces, while coarser grades are reserved for non-critical faces. Punch pins typically sit toward the finer end of that range because their working surface is in constant, repeated contact with the workpiece.
| Niveau d’arrivée | Approximation de Ra | Utilisation typique sur les goupilles de perforation |
|---|---|---|
| Fine/précision | ≤0,4–0,8 μm Ra | High-cycle stamping, tight-tolerance holes, matériaux abrasifs |
| Standard | 00,8–1,6 μm Ra | Estampage polyvalent avec comptage de cycles modéré |
| Grossier | >1.6 µm Ra | Opérations non critiques ou basse fréquence |
Comment obtenir la finition de surface de la goupille perforée
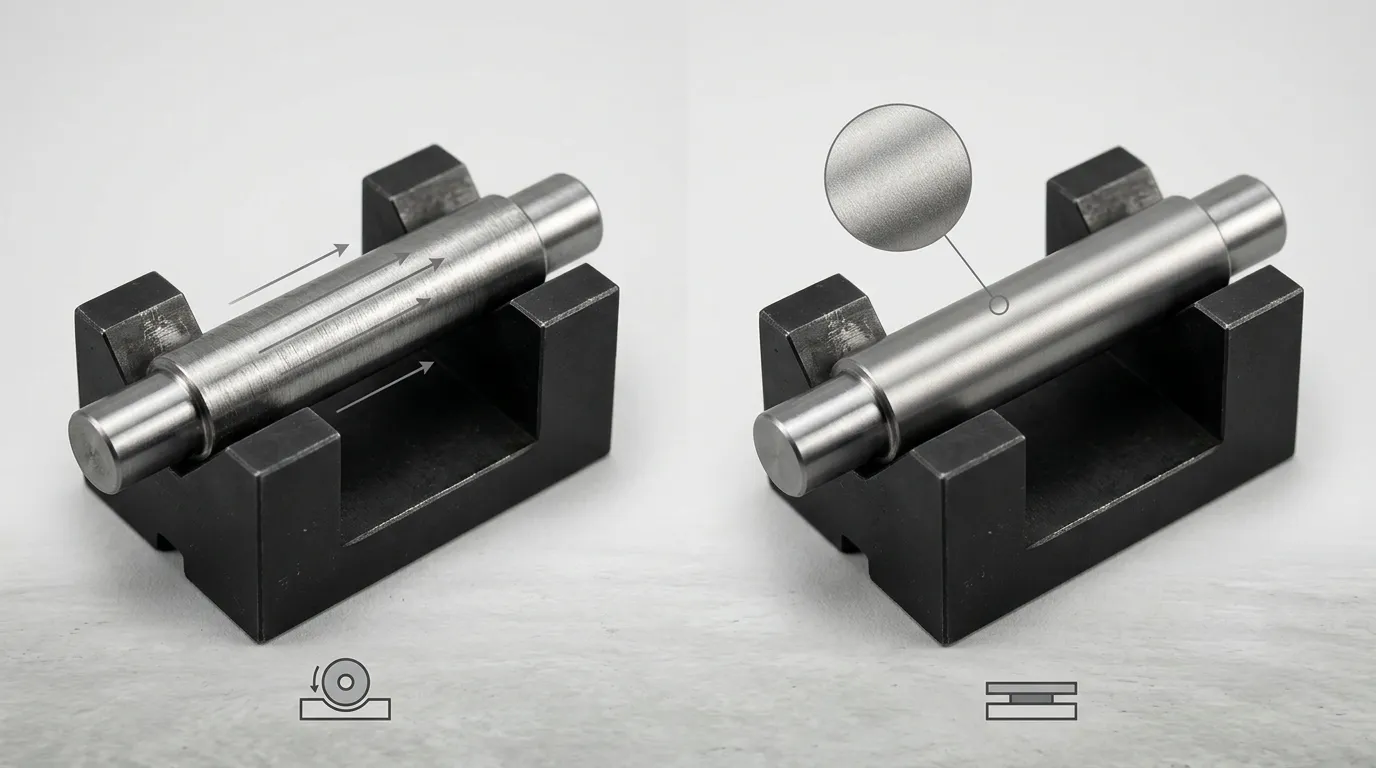
Two processes account for most punch pin finishing: grinding and lapping. Grinding removes material with an abrasive wheel and is typically applied along a specific orientation on the pin's working diameter; this orientation influences how the finish behaves under friction, since grind lines running parallel to the direction of material flow can affect how smoothly the slug slides off the tip. Lapping is a slower, finer-abrasive process usually reserved for tight-tolerance inner diameters or where an especially uniform, directionless finish is needed.
| Méthode | Application typique | Conséquences |
|---|---|---|
| Meulage | Surfaces de travail générales des goupilles de poinçon | Presque, repeatable finish; orientation-dependent friction behavior |
| Passages | Alésages à tolérance serrée ou faces de haute précision | Very fine, uniform finish with minimal directional pattern |
Neither process is inherently "better." The choice depends on the tolerance class, the pin's geometry, and whether the application is more sensitive to wear or to release performance.
Pourquoi la finition de surface détermine la durée de vie
Surface roughness has a direct, measurable relationship to wear. A rougher surface increases friction at the punch-workpiece interface, which accelerates material loss at the tip and along the working diameter with every stroke. Research on punching tool durability has shown that adhesive wear behavior is influenced by both surface roughness and the presence of low-friction coatings, confirming that finish is not a cosmetic detail but a performance variable, as documented in a Études universitaires sur la rugosité des surfaces et l’usure des outils de poinçonnage.
Finish alone does not determine wear resistance. Sunshine pairs its ground and lapped punch pins with a heat treatment process that increases hardness by roughly 30%, which works alongside the surface finish to extend service life rather than replacing the need for a controlled finish.
Pourquoi la finition de surface affecte la décharge propre de la pièce et du slug
Release performance is the second half of the finish equation, and it is easy to get backwards. A surface that is too rough can grip the slug or scrap material instead of letting it drop away cleanly, leading to double hits, jammed slugs, or marked parts. Less intuitively, a surface finish that is mismatched to the application, such as one that is inconsistent or improperly oriented, can also promote galling: localized adhesive transfer of material onto the punch surface that roughens it further and compounds the release problem over time.
Punch-die clearance plays a supporting role here. Even a well-finished punch pin can struggle with release if clearance is set incorrectly, though clearance itself is a separate design decision from surface finish and is covered in more depth elsewhere in our punching resources.
Adapter les exigences de finition aux conditions d’application
Rather than treating surface finish as a single fixed number, it helps to think in terms of what the application demands.
| Facteur d’application | Considération de la finition |
|---|---|
| High-cycle, continuous stamping | Privilégiez une finition plus fine pour ralentir l’usure plutôt que le volume |
| Matériau abrasif ou en feuille revêtue | Favor a finer, more uniform finish to reduce adhesive wear risk |
| Production basse fréquence ou courte durée | Une finition standard suffit souvent sans coût supplémentaire |
| Production de trous à tolérance serrée | Le rodage peut être préféré au meulage pour la constance |
These are general guidelines rather than fixed rules, since the correct finish for a given job depends on the specific material, Vitesse de pression, and tolerance class involved. For more information on how punching die design interacts with tooling choices, see our Guide des matrices de poinçon.
Une note sur les revêtements et les traitements résistants à l’usure
Coatings are sometimes used alongside surface finish to further reduce wear, since a smooth, well-finished substrate gives a coating a better surface to bond to. This is a general industry practice rather than a claim about any specific coating offered here, and buyers should confirm coating options directly with their tooling supplier.
Vérification de la finition de surface de la goupille de perforation
Once a finish requirement is set, it needs to be confirmed rather than assumed. Verification typically involves measuring roughness against the specified Ra value and checking that the finish is consistent across the working surface, not just at a single sample point. For a detailed walkthrough of what to check and how, see our Liste de contrôle pour l’inspection des goupilles de perforation.
Surface finish problems are also worth distinguishing from a separate but related failure mode: outright breakage. A worn or poorly finished punch pin degrades gradually, while breakage tends to be sudden and mechanical in origin. If you're troubleshooting a punch pin failure, our guide on Cassure de la poinçon dans les matrices d’emboutissage covers that distinct failure pattern.
Getting the surface finish right is less about chasing the smallest possible Ra number and more about matching the finish, and the process used to achieve it, to how the punch pin will actually be used. Checking your current tooling against the benchmarks above, and against the inspection checklist linked earlier, is a practical next step before specifying or reordering punch pins for your application.
Partager:



Écrit par Sunshine
Au soleil, Nous sommes un fabricant et fournisseur professionnel de composants de moule de précision, proposant une large gamme de produits pour les applications de stampage et de moulage par injection. Notre objectif principal est le poinçage des coins, Goupilles et manchons d’éjection, et poteaux guides et bagues. Avec un usinage CNC avancé, Contrôle qualité strict, et de fortes capacités de production, Nous garantissons une fiabilité, Pièces de haute précision, ainsi que des composants standards en stock pour un approvisionnement mondial rapide et efficace.
ACTUALITÉS
OBTENIR UN SERVICE
Avec des pièces de qualité adaptées à tous les budgets et un personnel accueillant formé pour rendre votre visite informative et sans tracas.
