



Goupilles de perforation pour emboutir en acier inoxydable: Matériaux et options de revêtement
There is no single best material or coating for punch pins used in stainless steel stamping. The right combination depends on the stainless grade and condition, Épaisseur de la feuille, Géométrie du poinçon, Volume de production, lubrication, L’alignement, Dégagement, and the failure mode already appearing in production.
A punch substrate provides the bulk toughness, Résistance à la compression, and edge support. Heat treatment establishes its usable hardness and fracture resistance. Surface finish affects friction and material pickup. The coating or surface treatment then modifies wear, Chaleur, and sliding behavior. Choosing only one of these elements rarely solves the complete problem.
This guide focuses on punch pins used to pierce or blank stainless steel sheet. It does not assume that the punch itself must be made from stainless steel. Pour des informations plus larges sur les types de puces, system-level material selection, Dégagement, Tolérances, et l’approvisionnement, voir le Guide des matrices de poinçon (déduit).
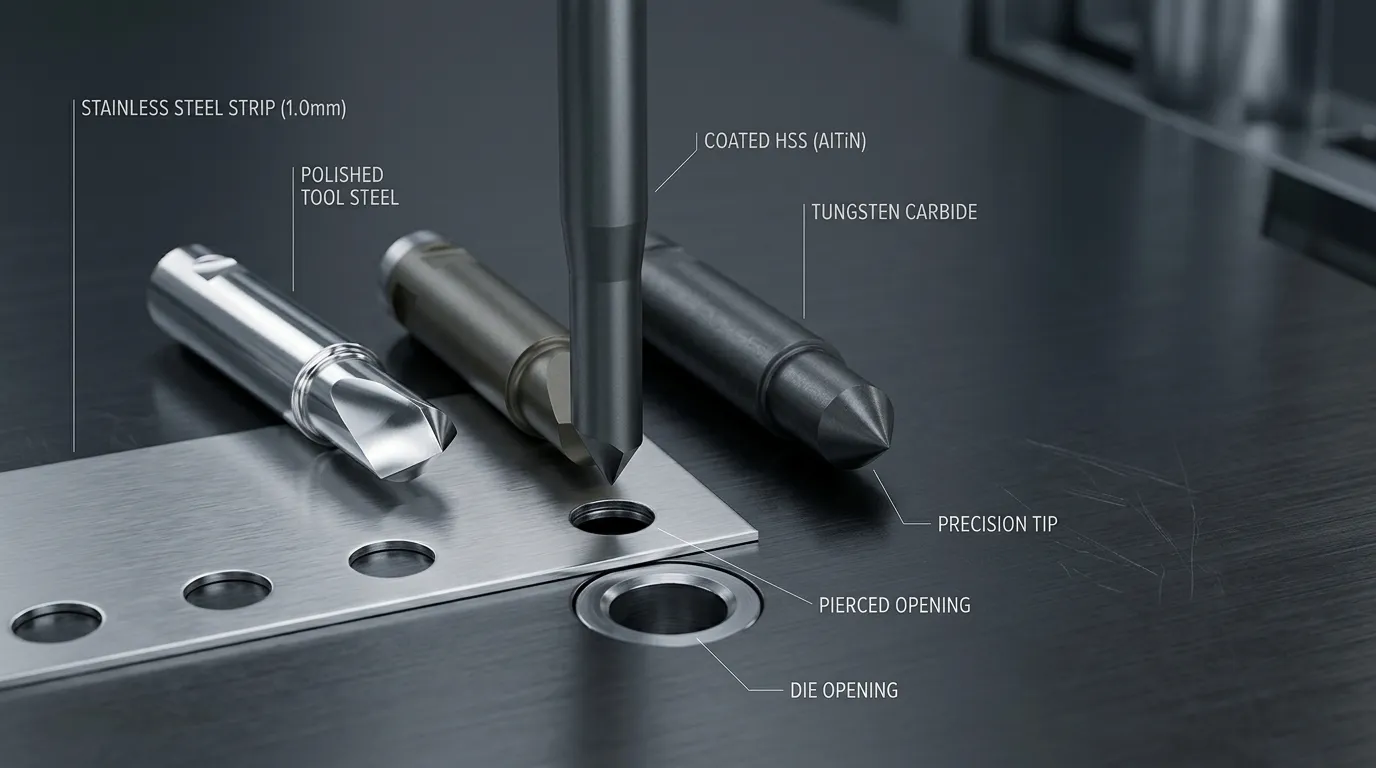
Pourquoi l’acier inoxydable modifie la sélection des goupilles
Stainless steel is not one uniform work material. Austenitic, ferritic, martensitic, and duplex grades have different mechanical properties and forming behavior. Le Aperçu de WorldStainless des familles d’acier inoxydable is useful background, but the tooling decision must go further than identifying the family name.
The supplier or tool engineer should know:
- the exact stainless grade;
- Épaisseur de la feuille;
- temper, Dureté, or tensile condition;
- Condition de la surface;
- pierced-hole or blank geometry;
- expected production quantity;
- lubrication method or restrictions;
- current punch material and coating;
- the actual failure seen in production.
Stainless applications often create high contact pressure, Friction glissante, and heat at the punch surface. Under unfavorable conditions, workpiece material can transfer onto the punch. This adhesive wear process is commonly described as galling or material pickup.
Une revue évaluée par des pairs de Gallage dans le formage des métaux explains that friction, Condition de la surface, Pression, Température, and wear development interact during the process. Once pickup begins, the roughened punch surface can attract more material, increase stripping force, damage the sheet surface, and accelerate further wear.
Stainless sheet may also work-harden near the cutting zone. Thicker or stronger material raises the load on the cutting edge. These conditions make it risky to choose a punch only by nominal hardness.
Choisissez le substrat de poinçon avant de choisir le revêtement
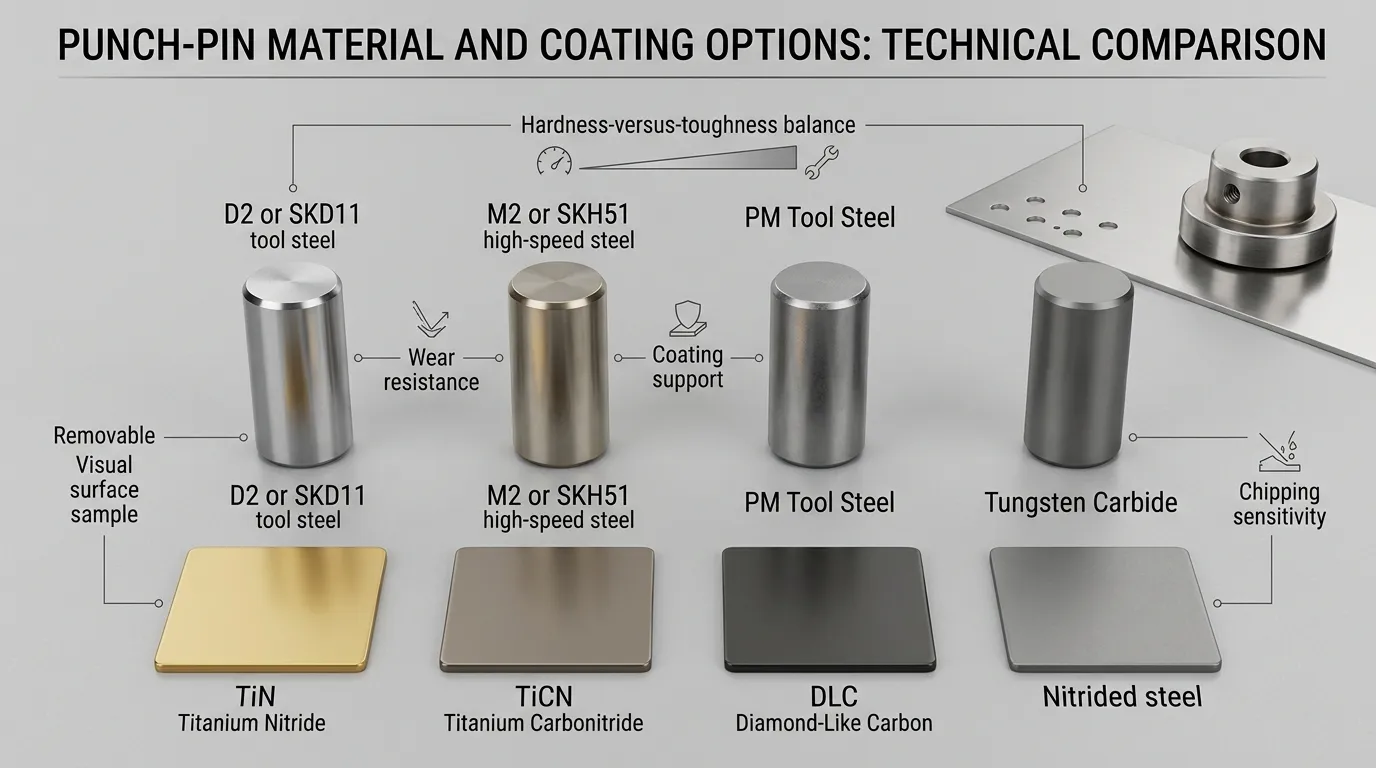
The coating is supported by the material underneath it. A hard coating on an unsuitable, poorly heat-treated, or damaged substrate can still crack, delaminate, Puce, or fail with the cutting edge.
The main punch-material options should be compared using several properties:
| Substrat à poinçon | Principaux points forts | Principales limitations | C’est une raison typique de l’envisager |
|---|---|---|---|
| Acier à outils de type D2 ou SKD11 | Résistance à l’usure, Résistance à la compression, Stabilité dimensionnelle | Can be less tolerant of impact, deflection, or sharp stress concentrations than tougher grades | Géométrie stable et production due à une usure modérée |
| M2, SKH51, or SKH9 HSS | Better balance of wear resistance, Robustesse, et résistance à la chaleur | Higher cost than conventional tool steel; still dependent on correct heat treatment | Stainless, thicker sheet, coated punches, or higher production demands |
| Acier à outillage PM | Un fort équilibre entre l’usure et la ténacité et une microstructure plus uniforme | Coût du matériau premium et exigences de traitement spécifiques à chaque catégorie | Lorsque l’acier conventionnel s’use trop vite mais que le carbure est trop cassant |
| Acier à outils résistant aux chocs | Forte ténacité et résistance aux fractures liées à l’impact | Résistance à l’usure plus faible que les grades fortement alliés | L’éclat ou l’impact est plus important qu’une usure progressive |
| Carbure de tungstène | Very high hardness, Résistance à la compression, et résistance à l’usure | Brittle under misalignment, choc, deflection, or poor edge support | Production stable à forte usure avec outillages rigides |
| Acier à outils inoxydable tel que SUS420 ou SUS440 | Résistance à la corrosion et polissabilité | Ce n’est pas automatiquement le meilleur substrat pour percer des feuilles en acier inoxydable | Environnements corrosifs ou applications où la poinçonne elle-même nécessite une résistance à la corrosion |
D2 or SKD11 for Stable, Wear-Led Applications
D2-class cold-work tool steel is widely used where wear resistance and compressive strength are important. Material documentation for BÖHLER K110, a D2-class steel, lists stamping and blanking among its applications and emphasizes wear resistance and dimensional stability.
D2 or SKD11 may be a reasonable starting point when:
- the punch has a robust cross-section;
- alignment and clearance are controlled;
- production volume is moderate;
- gradual wear is the main concern;
- sudden chipping or bending is not occurring.
It becomes a weaker choice when the punch is very slender, has sharp corners, experiences side loading, or breaks before the cutting edge wears out. Dans ces cas, additional hardness may make the problem worse rather than better.
M2, SKH51, or SKH9 When Toughness and Heat Resistance Matter More
High-speed steel is commonly evaluated when the punch needs a stronger balance of wear resistance, Robustesse, and resistance to heat generated during repeated cycling.
Conseils techniques de CONIC sur les matériaux d’outillage associates M2-type material with stainless steel, thicker sheet, coating use, and larger production quantities. That does not make M2 a universal answer, but it explains why HSS often appears in stainless stamping recommendations.
SunshinePro Perforatrice en acier à grande vitesse page lists SKH51 and SKH9 among its material options, along with vacuum heat treatment, Rectification de précision, EDM, and optional TiN or TiCN coatings. These are company-specific product options, not fixed specifications for every application.
HSS is worth evaluating when:
- D2 wears or chips too quickly;
- surface heat is significant;
- the punch will receive a PVD coating;
- production volume justifies a higher-cost substrate;
- the geometry needs more fracture resistance than conventional wear steel provides.
Acier à outils PM pour un meilleur équilibre usure-ténacité
Powder-metallurgy tool steels are useful when both wear and fracture resistance matter. Their more uniform microstructure can provide a better combination of properties than many conventionally produced tool steels.
Par exemple, the manufacturer describes BÖHLER K490 MICROCLEAN as a PM cold-work steel combining wear resistance, Résistance à la compression, Robustesse, and dimensional stability for applications that include stamping and blanking.
PM steel may be justified when:
- conventional D2-type steel wears too quickly;
- HSS does not provide the required service interval;
- carbide chips under the existing geometry or loading;
- downtime costs more than the material upgrade;
- repeated regrinding and stable dimensional behavior are important.
The recommendation must still be grade-specific. “PM steel” is a manufacturing category, not one standardized set of properties.
Carbide for Stable High-Wear Conditions, Not Every High-Volume Job
Tungsten carbide offers high hardness, Résistance à la compression, and resistance to abrasive wear. It can be effective in stable, high-volume applications where the punch receives rigid support and loading remains predictable.
Its main limitation is brittleness. Carbide is less forgiving of:
- Désalignement;
- Déviation du coup de poing;
- impact or interrupted loading;
- weak corner geometry;
- Soutien insuffisant;
- slug interference;
- Chargement latéral;
- Autorisation incorrecte.
A carbide punch that chips after a few cycles is not improved by selecting an even harder carbide grade without correcting the mechanical cause.
SunshinePro Punch au carbure page lists tungsten carbide, Rectification de précision, EDM, customized dimensions, and TiN, TiCN, or DLC coating options. Suitability still requires a review of the punch geometry, Pièce à travailler, Conditions de presse, et historique des défaillances.
Quand une poinçonne en acier inoxydable est en fait nécessaire
A punch used on stainless steel does not automatically need a stainless substrate.
Corrosion-resistant grades such as SUS420 or SUS440 may be selected when the tool itself is exposed to moisture, corrosive substances, frequent cleaning, or an environment where rust resistance matters. SunshinePro lists these grades on its separate stainless punch-pin product page.
That is a different engineering requirement from selecting a wear-resistant punch for stainless sheet. In many stamping applications, HSS, PM steel, conventional tool steel, or carbide may provide a more useful balance of wear, Robustesse, and edge stability.
Ajustez le revêtement ou le traitement de surface au mode de défaillance
Coating choice should begin with the observed surface failure.
- Usure de l’adhésif ou galure: prioritize low friction, resistance to material transfer, Préparation de surface, et lubrification.
- Usure abrasive: prioritize surface hardness and resistance to gradual material loss.
- High heat: review thermal stability and compatibility with the substrate’s heat-treatment condition.
- Chipping or fracture: correct the substrate, Géométrie, Alignement, or loading before focusing on the coating.
- Force de dénudage élevée: inspect pickup, Fin, lubrication, and punch withdrawal conditions.
A coating name alone is not enough. Performance also depends on coating thickness, Adhérence, Processus de dépôt, edge preparation, Dureté du substrat, Température de fonctionnement, et finition de surface.
TiN and TiCN Are Common Options, Not Universal Answers
TiN is one of the most familiar hard coatings used on tooling. It can improve wear resistance in suitable systems, but it should not automatically be described as the preferred stainless-steel coating.
Par exemple, Guidage de revêtement de Dayton Lamina assigns different treatments to adhesive wear, Usure abrasive, Chaleur, and specific work materials. Its recommendations also show that TiN is not universally preferred for stainless applications.
TiCN is commonly considered where higher wear resistance and improved sliding behavior are required. It may be evaluated for abrasive wear or material-pickup problems, but its performance still depends on substrate support, Préparation de surface, coating quality, et conditions de fonctionnement.
SunshinePro lists TiN and TiCN as available options on its HSS and stainless-steel punch-pin pages. The final selection should be based on the actual application rather than coating popularity.
AlTiN ou AlCrN pour les conditions liées à la chaleur
AlTiN and AlCrN coatings are often considered where elevated surface temperature and demanding wear conditions are central concerns.
Before selecting either coating, confirmer:
- the substrate’s tempering resistance;
- coating-process temperature;
- required friction behavior;
- edge preparation;
- Adhérence du revêtement;
- whether heat or galling is the dominant failure.
A heat-resistant coating will not correct an unsupported edge or a punch that bends under load.
DLC et systèmes multicouches lubricieux pour l’usure des adhésifs
DLC and other low-friction multilayer systems may be considered where adhesive wear, Irritant, and high stripping force dominate.
Conseils techniques de fabricants d’outillages tels que Mate Precision connects low-friction coating selection with lubrication restrictions, punch dimensions, Épaisseur de la feuille, and deflection. This is important because a lubricious surface can reduce friction, but it cannot stabilize a weak punch geometry.
DLC suitability depends on the substrate, Processus de dépôt, service temperature, Adhérence du revêtement, and edge loading. SunshinePro lists DLC on its carbide-punch page, but that does not confirm availability or suitability for every punch material.
Nitruration lorsqu’un traitement de diffusion correspond au plan de service
Nitriding hardens the punch surface by diffusion rather than adding a separate deposited layer. It can be useful where surface hardness and geometry coverage are important.
Its selection should consider:
- substrate compatibility;
- Profondeur de cas;
- Finition de surface requise;
- Changement dimensionnel;
- Allocation de rectification;
- whether the treated layer will remain after sharpening.
Nitriding should not be described as a SunshinePro capability unless confirmed for the specific order. It remains a general technical option to discuss with the tooling and treatment supplier.
Diagnostiquer la panne avant de mettre à niveau l’outil
A more expensive material or coating is useful only when it addresses the actual failure.
| Symptôme observé | Likely mechanism | Vérifiez avant de passer à niveau | Direction possible du matériau | Possible surface direction |
| Accumulation d’inox sur le poinçon | Usure par la galère ou l’adhésif | Fin, lubrication, Chaleur, Dégagement, stripping action | Conservez un substrat dur s’il ne se déforme pas ou ne s’écaille pas | Low-friction PVD, DLC-type system, Nitrage, or improved polishing depending on conditions |
| Arrondi progressif des arêtes | Usure abrasive | Workpiece condition, Dégagement, punch hardness, Volume de production | HSS, PM steel, or carbide if the process is stable | TiCN ou un autre revêtement axé sur l’usure |
| Petits éclats à la tranchante | Fracture locale ou ténacité insuffisante | Géométrie des arêtes, Alignement, Angles, Support de la perforation, Traitement thermique | Tougher HSS, PM steel, or shock-resistant steel | Ne considérez pas le revêtement comme la solution principale |
| Rupture soudaine du poinçon | Mechanical overload, deflection, Désalignement, or brittle substrate | Orientation, Serviteur, Dégagement, slug interference, Longueur du poinçon | Substrat mené par la ténacité après correction de la cause mécanique | Le revêtement est secondaire |
| Déformation ou roulement des arêtes | Inadequate hardness, Résistance à la compression, ou support | Traitement thermique, punch load, Épaisseur, Géométrie | Higher-strength tool steel, HSS, PM steel, or carbide where stable | Usure du revêtement seulement après correction du substrat |
| Forte force de retrait | Micro, poor stripping, Finition rugueuse, or inadequate lubrication | Stripper condition, punch surface, lubrifiant, Chargement latéral | Maintenir une ténacité suffisante pour la charge de retrait | Traitement à faible friction lorsque compatible |
Le diagnostic général de fracture doit figurer dans le guide séparé de Cassure de la poinçon dans les matrices d’emboutissage. The critical point here is that chipping and breakage often indicate a bulk-material or mechanical problem, not a missing coating.
Vérifiez la géométrie et les conditions de la matrice avant de blâmer le matériau
The punch operates as part of a complete die system. Before changing the substrate or coating, inspect the conditions that control how the load reaches the cutting edge.
- Confirm punch alignment. Misalignment creates uneven edge loading and can chip even a premium punch.
- Review punch-and-die clearance. Clearance should match the workpiece material and thickness. An unsuitable value can increase force, Formation de la meule, Usure, and fracture risk.
- Inspect the stripper and guide system. Poor guidance or abnormal stripping can bend the punch during withdrawal.
- Check the retainer and mounting condition. Movement at the head or shank changes how the punch is loaded.
- Inspect for slug interference. A trapped or pulled slug can create sudden overload.
- Review the punch surface. Grinding marks, Dégâts, or pickup can accelerate galling.
- Confirm lubrication. Restricted lubrication changes the friction and coating requirements.
- Account for coating thickness. Final dimensions and tolerances should reflect the complete coated condition.
Le Guide des composants de la puce provides broader information about punches, Quilles, Silents, Composants du guide, and wear parts.
Les petits coups de poing fins ont besoin d’une critique de robustesse d’abord
A small-diameter or high-aspect-ratio punch can deflect before the cutting edge reaches its nominal material limit.
Risk rises when the punch has:
- longueur excessive sans support;
- Coins vifs;
- Sections étroites;
- Chargement latéral;
- interrupted contact;
- Mauvaise orientation;
- heavy stripping force.
In this situation, selecting carbide or maximizing hardness can increase chipping risk. A tougher HSS or PM steel, longueur plus courte sans support, stronger guidance, and improved corner design may provide a better result than a harder coating.
Utilisez les conditions d’application pour présélectionner le système matériau–revêtement
The following matrix provides a starting direction, not a final engineering specification.
| Conditions d’application | Direction du substrat à évaluer | Direction de surface à évaluer | Vérifiez d’abord |
| Moderate volume, robust geometry, controlled process | D2/SKD11 ou HSS | Polished uncoated surface, TiN, TiCN, or nitriding depending on wear | Grade, Épaisseur, Dégagement, lubrication |
| Usure abrasive à fort volume | HSS, PM steel, ou carbure | Traitement du DPV axé sur l’usure | Alignement, edge support, regrinding plan |
| Gallage avec micro de matériau visible | Acier HSS ou PM résistant si le substrat reste stable | Low-friction PVD, DLC-type system, multilayer coating, or nitriding | Fin, lubrifiant, Chaleur, stripper action |
| Petite ou fine poinçon avec éclat | Tough HSS, PM steel, or shock-resistant steel | Le revêtement n’est qu’après avoir contrôlé la cause de la fracture | Unsupported length, Orientation, Angles, Alignement |
| Feuille en acier inoxydable épaisse ou à haute charge | HSS or PM steel; carbide only in a rigid, stable setup | Chaleur- and wear-appropriate coating | Punch load, Dégagement, Soutien, État de presse |
| Environnement d’outil corrosif | Acier inoxydable résistant à la corrosion lorsque la charge le permet | Traitement compatible avec le substrat inoxydable sélectionné | La priorité principale est que la résistance à la corrosion ou la performance au poinçon soit la priorité principale |
Do not use this matrix to skip testing or drawing review. Two applications using the same stainless grade may need different punches because the thickness, Diamètre du trou, Longueur du poinçon, lubrication, Vitesse de pression, and service expectations are different.
Comparez les options d’outillages par facilité de service et coût par impact
Initial purchase price is a weak basis for comparing punch options.
A more useful evaluation includes:
- hits between sharpening or replacement;
- unplanned downtime;
- tool-change frequency;
- regrinding cost;
- recoating feasibility;
- dimensional loss after sharpening;
- scrap and surface-damage risk;
- inspection time;
- Délai de livraison pour remplacement;
- probability of sudden fracture.
A PM steel or carbide punch may cost more at the start but reduce cost per hit in a stable application. The same upgrade can become expensive if the punch continues to break because of misalignment or poor guidance.
Regrinding also changes the tool. It can reduce punch length, remove the treated surface near the cutting edge, alter corner geometry, and affect shut height or penetration. Recoating is possible only when enough usable material remains and the surface can be restored to the condition required by the coating supplier.
The service plan should therefore be considered before the original material and coating are selected.
Informations à inclure dans une RFQ personnalisée pour broches de perforation
A supplier cannot make a defensible recommendation from the phrase “punch for stainless steel” alone.
Include the following information in the request:
- stainless grade and family;
- Épaisseur de la feuille;
- temper, Dureté, or tensile condition;
- part and hole drawing;
- Diamètre du poinçon, Longueur, Tête, Shank, and corner geometry;
- required dimensional tolerances;
- die clearance where known;
- press type and stroke rate;
- Volume de production attendu;
- target service interval;
- lubricant or dry-running restriction;
- current punch material and hardness;
- current coating or treatment;
- photographs or samples of wear, micro, Ébréchage, or breakage;
- regrinding and recoating expectations;
- Matériel requis, Dureté, dimensionnelle, ou documentation de revêtement.
SunshinePro states that it supplies standard components and non-standard customized parts processed from customer drawings. Its relevant punch pages list combinations of CNC machining, Rectification de précision, EDM, Traitement thermique sous vide, custom dimensions, HSS, carbure, stainless tool steel, and selected coating options.
These website-confirmed capabilities should still be reviewed against the actual drawing and application. A tolerance or material listed on one product page should not be assumed to apply to every punch geometry.
Principe de sélection finale
Use this order when selecting punch pins for stainless steel stamping:
- Identify the stainless grade, Condition, Épaisseur, and feature geometry.
- Determine whether the current failure is galling, Usure abrasive, Ébréchage, Casse, ou déformation.
- Correct alignment, Dégagement, Orientation, Fin, Démontage, and lubrication problems.
- Select the substrate for bulk toughness, Résistance à la compression, and edge stability.
- Select the coating or treatment for the dominant surface failure.
- Compare serviceability, Temps morts, and cost per hit.
- Confirm the final system through drawing review and application-specific validation.
For a custom review, Soumettre le dessin, stainless specification, Conditions de production, and current failure details through SunshinePro’s Page de contact. That information gives the supplier a practical basis for evaluating the punch material, Traitement thermique, Fin, Revêtement, et exigences d’inspection.
Partager:



Écrit par Sunshine
Au soleil, Nous sommes un fabricant et fournisseur professionnel de composants de moule de précision, proposant une large gamme de produits pour les applications de stampage et de moulage par injection. Notre objectif principal est le poinçage des coins, Goupilles et manchons d’éjection, et poteaux guides et bagues. Avec un usinage CNC avancé, Contrôle qualité strict, et de fortes capacités de production, Nous garantissons une fiabilité, Pièces de haute précision, ainsi que des composants standards en stock pour un approvisionnement mondial rapide et efficace.
ACTUALITÉS
OBTENIR UN SERVICE
Avec des pièces de qualité adaptées à tous les budgets et un personnel accueillant formé pour rendre votre visite informative et sans tracas.
